
Aluminum coating adhesion should be purchased with an identified coating system, an agreed test method and a written acceptance requirement. A report that says only “adhesion passed” leaves the buyer unable to tell what was checked or which supplied parts the result represents.
Begin with the report’s scope. A surface appearance approval, a coating thickness result and an adhesion assessment answer different questions. Keep each requirement visible in the order so one favorable result does not stand in for every finishing check.
On this page
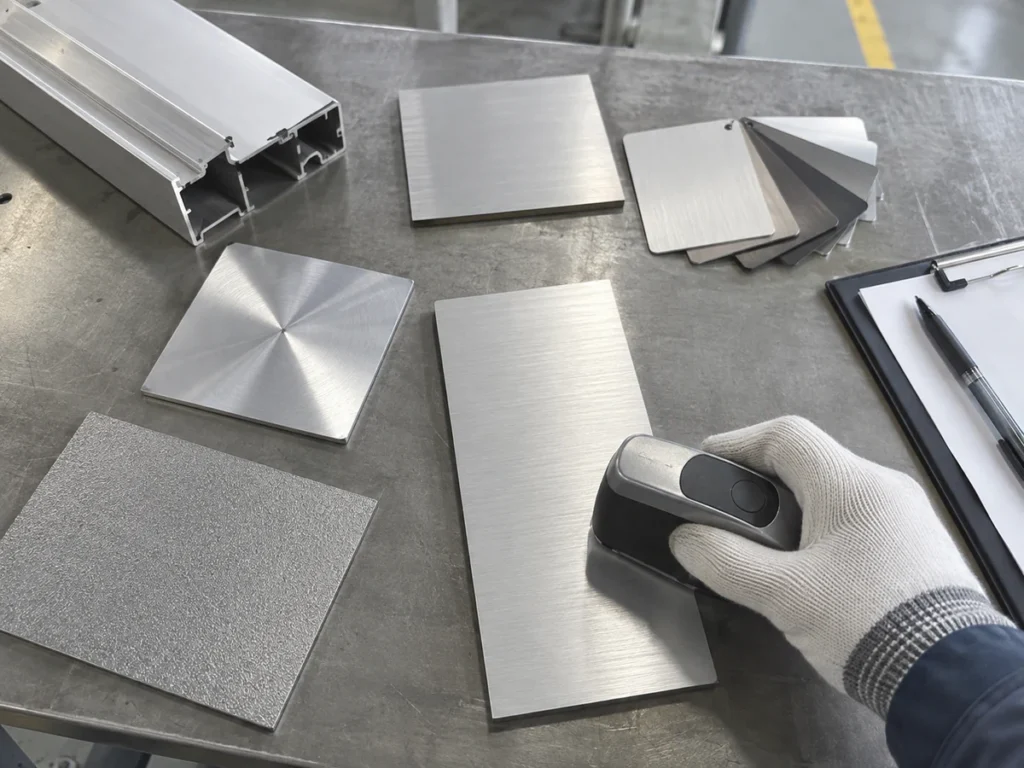
1. Name the aluminum coating adhesion method
Request the complete test designation, edition and applicable method. Avoid replacing it with an informal phrase such as “tape checked.” Send the project requirement to the finishing and inspection teams before samples are prepared.
The public scope of ASTM D3359 describes tape-based ratings for relatively ductile coating films on metallic substrates. Its significance section explains that the rating does not make fine distinctions between higher levels of adhesion.
The public abstract of ISO 2409 describes a cross-cut assessment of resistance to separation. It explicitly distinguishes that assessment from a measurement of adhesion. ASTM also states that D3359 is not technically equivalent to ISO 2409.
Keep those distinctions in the quotation comparison. If one supplier offers an ASTM-based assessment and another an ISO-based assessment, ask the responsible quality team whether each meets the specified requirement. A similar-looking pattern on a sample is insufficient grounds to accept an unreviewed substitution.
Make the inspection scope part of the quote
Identify who performs the work, which report is supplied and whether the quoted scope includes the required verification. If a supplier excludes the requested assessment, record that exclusion before placing the order.
This guide summarizes purchasing questions from public technical information. It does not reproduce the standards’ procedures. The inspection team should work to the applicable complete method and approved project instructions.
2. Identify the coated sample and its delivery stage
Record the part number, drawing revision, material identity, coating reference and batch or order reference. Ask whether the tested item is a finished component, a separately prepared panel or another agreed specimen.
When a panel accompanies a component order, have the responsible team explain the scope that panel represents. Keep that explanation with the report. Do not let an unidentified sample become a general approval for every profile, panel or coating variation in the shipment.
State the coating system requested for the actual part. Where the project specifies preparation, primer, topcoat or a particular product reference, retain those fields in the released documents. Record proposed substitutions separately and obtain the required technical review.
Use a simple sample identity record
- Part: item number and drawing revision.
- Finish: agreed system and specification reference.
- Sample: specimen identity and relationship to the order.
- Stage: condition when submitted for the specified assessment.
- Record: report identifier and inspecting organization.
These are administrative fields, not a laboratory procedure. Their purpose is to let a purchaser follow a result back to the object and requirement it concerns.
If you are still selecting the finishing route, start with the anodizing and powder coating comparison. Define the actual finish first; this article does not assign one adhesion test to every aluminum surface treatment.
3. Read the result format and failure location
A classification and a pull-off strength result use different reporting formats. Keep the method beside the result rather than converting one into the other.
DeFelsko’s adhesion testing overview explains that pull-off testing loads a fixture bonded to the coating and reports strength in pressure units such as MPa or psi. Separation occurs at the weakest plane in the combined fixture, adhesive, coating and substrate system.
The same overview identifies several fracture locations: at an interface, within a coating or substrate, or in the fixture adhesive. It also cautions that results obtained using different devices or substrates with different stiffness may not be comparable.
For a pull-off report, read the recorded failure description alongside the number. Ask the inspecting team to interpret any fixture adhesive separation and explain whether the result satisfies the agreed reporting and acceptance scope.
Separate observation from the decision
A useful review record has space for the supplied result, the relevant requirement and the decision made by the authorized reviewer. Preserve the original laboratory report instead of replacing it with a supplier’s short summary.
For a tape assessment on a multilayer coating, ASTM notes that separation between layers may not determine the coating-to-substrate adhesion. Read the stated failure location and scope before treating the report as evidence for an interface it did not assess.
If a report is incomplete, request the missing information. A purchaser should not infer the standard edition, invent a result unit or choose a favorable interpretation from an unclear photograph.
4. Agree the acceptance rule before production
The order should identify the required assessment and the acceptance criteria set by the responsible project team. Do not insert a universal passing grade into every RFQ. The intended application and released specification determine what evidence is required.
Ask whether the supplier has accepted that requirement without exclusions. Resolve a proposed alternative before production, and retain the approved revision in the purchasing record.
Close the report review in this order
- Match the report to the identified sample and coating requirement.
- Confirm that the reported method meets the released inspection scope.
- Read the result and relevant observations without changing the original record.
- Have the authorized reviewer apply the agreed acceptance rule.
- Record release, hold or the next clarification needed.
If two reports disagree, preserve both. Check their sample identities and assessment scopes, then agree the next review step. Selecting the better-looking result without resolving the difference leaves the order’s acceptance basis unclear.
A first article inspection record can keep dimensional and finishing approvals together while preserving their separate requirements. One approval field should not silently close another outstanding check.
Prepare the cutting-to-finishing handoff
Give each supplier the current drawing, cut quantities, required end condition and finish scope. Identify which operations are completed before coating and who supplies the agreed finishing documentation.
List any faces, holes or contact areas that require special treatment in the project documents. The masking requirement guide addresses how to communicate those areas clearly. Keep the finishing team’s approved process instructions separate from the cutting list.
For the blank preparation stage, review the cutting before powder coating guide. Retain part identities through the handoff so reports can be associated with the correct finished order.
Buyer questions
Does a smooth-looking coating prove adhesion?
Appearance review alone does not supply the result of the specified adhesion assessment. Keep the required test evidence and visual acceptance record as separate order fields.
Are ASTM D3359 and ISO 2409 interchangeable?
Do not assume equivalence. Confirm the applicable designation with the responsible quality team and obtain approval for a proposed method change.
Can a passing sample approve every later shipment?
Only use a report for the scope it identifies and the acceptance arrangement agreed for the order. Preserve sample and batch identities rather than extending the approval without review.
Should a coating report replace dimensional inspection?
No. The finishing record and the drawing inspection address separate requirements. Keep both in the release package when both are specified.
Discuss the aluminum cutting stage
Contact JiurunCut with the aluminum section drawing, cut lengths, quantities and required end condition. Include the finishing handoff and documentation scope so the cutting review starts from the correct requirements.