
Aluminum cutting rework needs a clear route from a held part to a documented release. A second operation may address a problem, but the part still needs the agreed checks before it returns to a usable batch. Keep the original condition, approved action and final result connected.
For buyers, this is a useful topic during sample reviews and production handovers. Ask how a supplier identifies affected pieces, approves the work and confirms the remaining requirements. These five checks help you discuss the process without assuming every cutting problem can be corrected.
Start with three decisions
- Identify the affected part and requirement before authorizing work.
- Review the proposed action and every feature it could affect.
- Count released pieces separately from pieces processed again.
On this page

Check 1: record the aluminum cutting rework condition
Describe what prompted the hold. “Needs fixing” gives the next person little to assess. State the part identity, drawing revision, affected feature, observed condition and requirement being reviewed. Attach photographs or measurement records where they help explain that specific condition.
The ASQ quality glossary describes a nonconformity as a requirement that has not been fulfilled. It also describes a nonconforming record as a lasting account of the condition. That terminology supports keeping the original issue visible while the team decides what happens next.
Separate a confirmed issue from an unexplained reading. If the measuring method, datum or drawing interpretation is uncertain, resolve that uncertainty before selecting an operation. A cutting change based on the wrong reference can introduce another problem instead of settling the first one.
Keep the affected pieces identifiable during review. Use the site’s established hold and tracking process, including any approved method for separating them from released stock. Avoid marks or handling that could damage a visible finish or confuse the part identity.
Check 2: approve a specific plan before work starts
A useful plan names the affected pieces, proposed operation, responsible person, required resources and checks after the operation. It should reference the applicable drawing and the approval needed under the buyer’s and supplier’s agreed procedures.
Do not treat an informal instruction to “trim it again” as a complete plan. Clarify which end would change, how the finished requirement will be assessed and whether sufficient material remains. The responsible technical reviewer needs to decide whether the proposed action is suitable for that part.
If the action would leave the part outside the approved requirements, route the decision through the appropriate approval process. Record the resulting disposition clearly. Avoid presenting a changed requirement as though the original part requirement had been met.
Ask who is allowed to approve the operation and who is allowed to release the result. These roles may sit with different people. The article’s workflow is a discussion aid; the actual authority and documentation come from the procedures and agreements for your order.
Check 3: review the features the action could affect
Look beyond the feature that first triggered the hold. Removing material from an end can change finished length and the relationship between that end and existing holes, slots or mating faces. Review those relationships against the drawing before approving the work.
A profile member may have an identified left and right end, a visible face and an assembly orientation. Preserve those identities through the proposed operation. A piece that looks similar after turning around may still have a different relationship to its features.
Consider surface protection and the next manufacturing stage. Another handling or clamping operation could affect surfaces that matter to the buyer. State what needs protection and inspection rather than assuming that a dimensional correction settles every acceptance question.
For reference relationships, use the hole-position review alongside the drawing. This helps the discussion cover the distance from the approved datum, not just the appearance of the new end face.
Check 4: reinspect against the agreed requirements
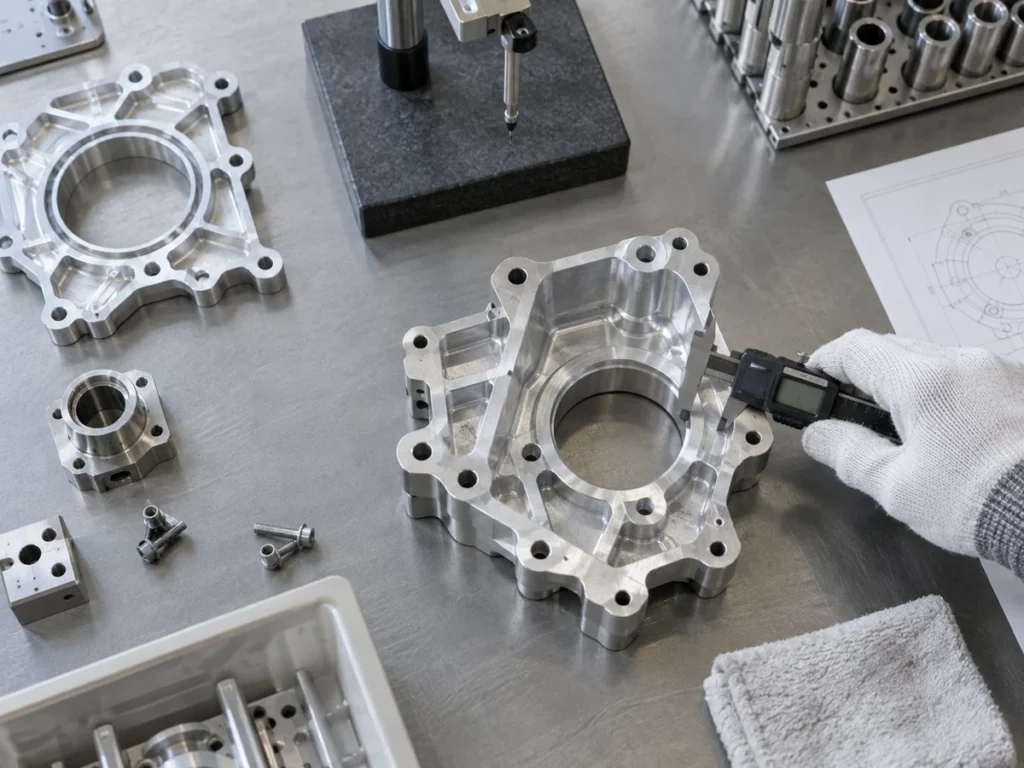
Define the reinspection before processing the pieces. Identify the characteristics to check, the reference surfaces, suitable measurement method and records to retain. Include characteristics that the proposed work could affect as well as the original issue.
The previous measurement record remains useful context, but it describes the previous condition. Record the result after the approved work with the correct part identity and revision. If a piece remains uncertain, keep that uncertainty visible instead of treating the operation itself as acceptance.
Use the inspection plan agreed for the order. Do not assume a universal sample quantity or an automatic requirement to measure every dimension on every piece. The appropriate extent depends on the requirements, affected characteristics and applicable process.
Match the tool to the feature and method. The cutting-gauge checklist explains why a tool’s identification and applicability need review. A convenient gauge or caliper reading should answer the intended question under a defined method.
Check 5: reconcile the release and remaining holds
Close the loop with quantities and identities. How many pieces entered the hold, how many received the approved work, how many completed reinspection and how many were released? Keep these counts distinct so the next stage knows what it can actually use.
Record the release decision through the agreed authority. Include any remaining holds or other dispositions and the location of the pieces. A supervisor seeing a full rack should be able to connect its labels to the current status without relying on a verbal explanation.
Keep the production records linked. The batch-traceability guide provides a starting point for connecting the stock identity, cutting record and later decisions. Rework should add to that history rather than erase the original event.
A ten-piece review: processed does not yet mean released
This is a fictional count example, not a test result or a production claim. Ten identified members are held for review. A responsible reviewer approves a specific rework plan for six of them. The other four remain held while their disposition is considered.
| Recorded state | What the count means |
|---|---|
| Ten initially held | Ten pieces need a documented decision. |
| Six authorized for the plan | The plan applies to those six identified pieces. |
| Six processed again | The operation is complete; release remains to be recorded. |
| Four still held | They have no release from this rework plan. |
No released quantity is given in this example because no reinspection result has been specified. The team cannot fill that gap by copying the number processed. It must record what the checks and release decision establish for each applicable piece.
This distinction also matters for a kit. Releasing several members does not necessarily create a complete set if the remaining held member is required for assembly. Reconcile the relevant part identities before promising a complete delivery.
Connect the result to preventing recurrence
Resolving the affected pieces and addressing why the issue happened are separate actions. Keep a usable record of the original condition, investigation and subsequent changes. A completed rework entry alone does not demonstrate that recurrence has been prevented.
During a machine review, discuss the verified issue in context: profile identity, drawing, stock support, cutting references, handling and inspection method. Ask what evidence would help evaluate a proposed change. Avoid assigning the cause to the saw before the investigation supports that conclusion.
Send JiurunCut the representative profile drawing and cutting requirements for a machine-selection discussion. Explain which feature needs review and what the downstream part requires. Confirm the scope of any proposed sample evaluation rather than assuming a repair or rework service is included.
Buyer questions about cutting rework
Can every nonconforming cut part be reworked?
No. The responsible reviewer needs to assess the actual condition and proposed action against the requirements. Some pieces may have no suitable route back to the required condition. Keep the resulting decision documented.
Should the original inspection record be replaced?
Preserve the original condition and link the later operation and reinspection records to it. This makes the sequence understandable and helps the next reviewer distinguish earlier observations from the final release decision.
Does repeating the cut count as corrective action?
It describes an operation on an affected part. To address recurrence, review the cause and the effectiveness of the resulting process changes separately. Do not use the number reworked as proof that the underlying issue is solved.