
A powder coating gloss level should include the measurement angle and an agreed acceptance range. Keep those fields with the coating identity, reference sample and measured face. A description such as matt or satin helps explain the intended appearance, but the inspection record needs a defined comparison.
For an aluminum frame or housing, the buyer should be able to answer three questions: what finish was ordered, how its gloss is evaluated and which result supports release. This guide turns those questions into three connected records.
Read a gloss value as a complete statement
- Record gloss units, commonly written GU.
- Retain the measurement geometry, such as 60°.
- Identify the face, reference and agreed limits.
On this page
What a powder coating gloss level describes
A glossmeter evaluates reflected light using a defined geometry. Elcometer’s gloss measurement guide explains gloss units as a comparison with a polished glass reference. The measurement angle and surface properties affect the result.
Its guide starts angle selection with a 60° measurement and describes using 20° for high-gloss evaluation and 85° for low-gloss evaluation. Keep the actual required method on the order. These angle descriptions do not create a universal acceptance range for a powder-coated aluminum part.
GU and percent reflectance are different report labels. Do not rewrite 40 GU as 40% simply because the number is convenient. Retain the unit and angle supplied by the approved method.
ASTM’s public D523 scope describes specular-gloss measurement of nonmetallic specimens using 20°, 60° and 85° geometries. Its public description also distinguishes other appearance aspects, including texture and reflection haze. The complete applicable method and customer requirement remain necessary for an actual inspection.
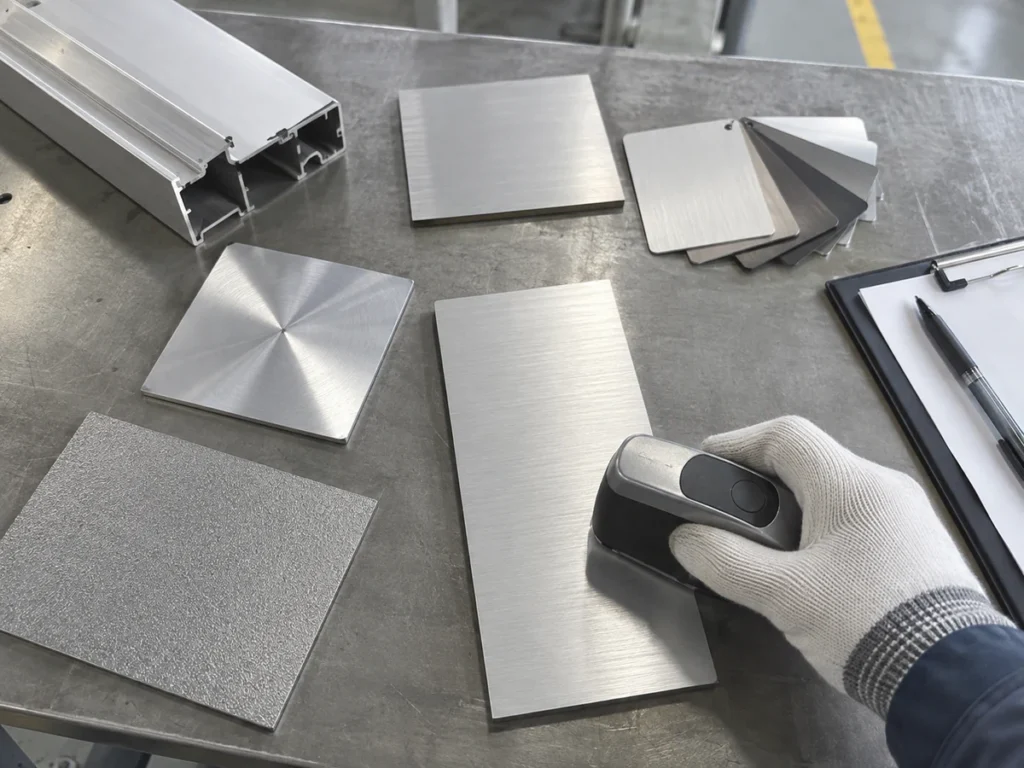
Record 1: identify the ordered finish
Keep the coating manufacturer, product designation, color reference and required surface texture together. Add the specified gloss method and limits. Identify the drawing revision and the stage at which the requirement applies.
If the order uses an approved physical sample, give it a sample number and approval status. State what it represents: a finish panel, a particular part face or an assembled appearance reference. Keep an exploratory sample separate from a released order reference.
A color code and a gloss requirement answer different questions. Two offers can repeat the same color code while proposing different gloss or texture. Our powder coating color match guide covers the broader appearance brief.
Mark the visible faces on the part drawing. If adjoining rails need a consistent appearance, identify them as a group. Receiving should not have to choose an arbitrary hidden face because the intended surface is difficult to locate.
Record 2: define how the surface will be measured
Retain the agreed method reference and edition, measurement geometry, instrument identity and applicable calibration information. Ask the responsible inspection team to define the procedure for the actual coating and part.
Identify the measured area, instrument orientation and surface condition. For a narrow rail, curved face or recessed surface, ask how the approved method can be applied. A reading from a convenient flat panel should not silently become a result for an inaccessible part face.
If a representative panel is used, record how it relates to the supplied parts and what the agreement permits it to demonstrate. Keep the panel identity connected to the coating and delivery group. It is useful only within that defined scope.
Agree the locations and number of readings required by the inspection plan. State whether acceptance applies to each reading, an average or another specified result. A numerical limit without that rule can lead to conflicting receiving decisions.
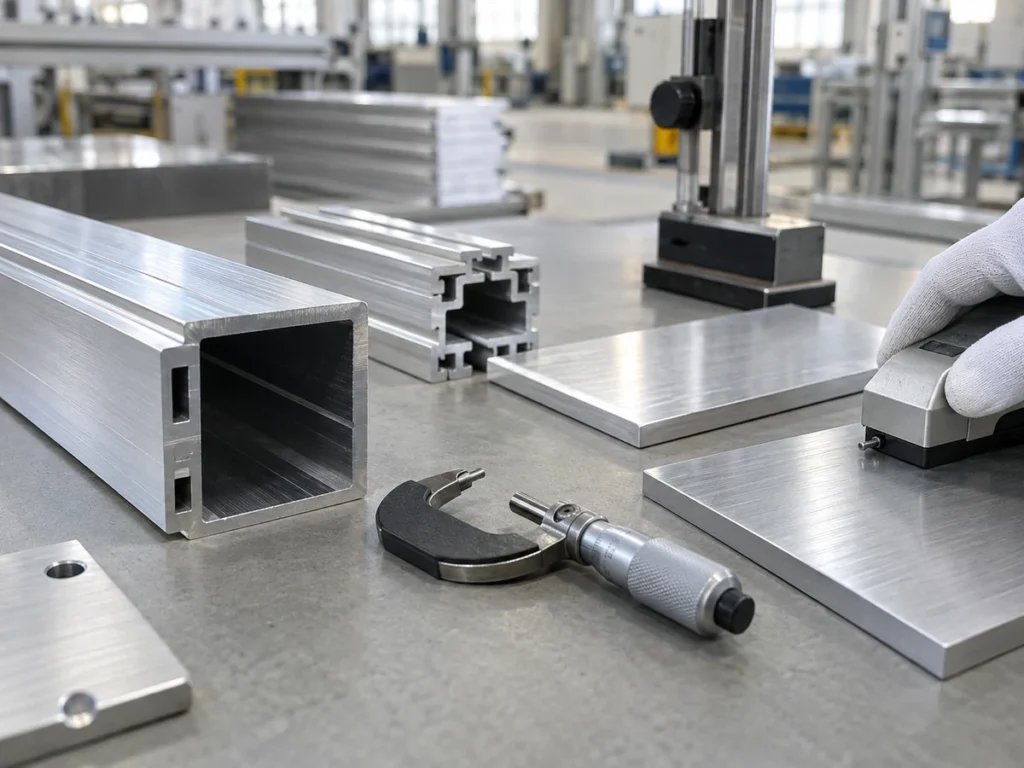
Record 3: report the value with its context
Each result should identify the part or sample, delivery group, measured face, location, angle and GU reading. Retain the relevant conditions and any departures from the agreed procedure.
| Short report entry | What remains to clarify |
|---|---|
| Gloss: 40 | Unit, geometry, face and acceptance rule. |
| 40 GU at 60° | Sample identity, location and applicable limits. |
| 40 GU at 60° on face A | Part revision, method and documented release decision. |
Keep a receiving concern descriptive while it is investigated. A changed value alone does not identify the cause. Ask the coating supplier and quality owner to review the actual surface, method and reference.
Also keep gloss separate from coating thickness, adhesion and the required service performance. One appearance result does not complete every coating requirement. The coating adhesion guide explains a separate test and acceptance discussion.
A fictional receiving comparison
Assume an invented order defines 40 ± 5 GU at 60° on visible face A, with each required location judged separately. The lower and upper limits are 35 and 45 GU. This is an arithmetic example, not a recommended specification.
Fictional readings of 38 and 44 GU fall inside that numerical interval. A third reading of 46 GU lies above it. Their average is approximately 42.67 GU, but that average does not satisfy the assumed rule that every required location must meet the limits.
Now suppose a second report gives 44 GU at 20°. Its number cannot simply be checked against this 60° requirement. Ask for the required measurement or an explicitly approved alternate comparison.
These statements explain documentation and arithmetic. They do not establish actual part acceptance, a validated inspection or the cause of an appearance difference. The real decision follows the complete approved method and requirement.
Connect the cutting and finishing stages
State whether cutting occurs before the specified coating or on already finished stock. Mark the surfaces to protect and identify the required cut-end condition. Keep the relevant handling and packing instructions with the cut list.
Send JiurunCut the section drawing, finish route and surface requirements to discuss cutting and handling. Have the coating and quality teams define the finish process and its acceptance record.
Buyer questions
Does a color code specify gloss?
Keep gloss, texture and coating identity explicit alongside the color reference. A shortened color line leaves those requirements unclear.
Can readings at different angles be compared directly?
Retain each geometry and use the approved comparison method. A matching number at a different angle does not establish compliance.
Can a photograph establish a GU value?
No. Use the required instrument method and identified surface. A photograph can communicate a concern but does not supply that measurement.
Does a matching gloss value prove coating quality?
It addresses a defined appearance requirement. Thickness, adhesion, damage and service requirements need their own applicable evidence.