
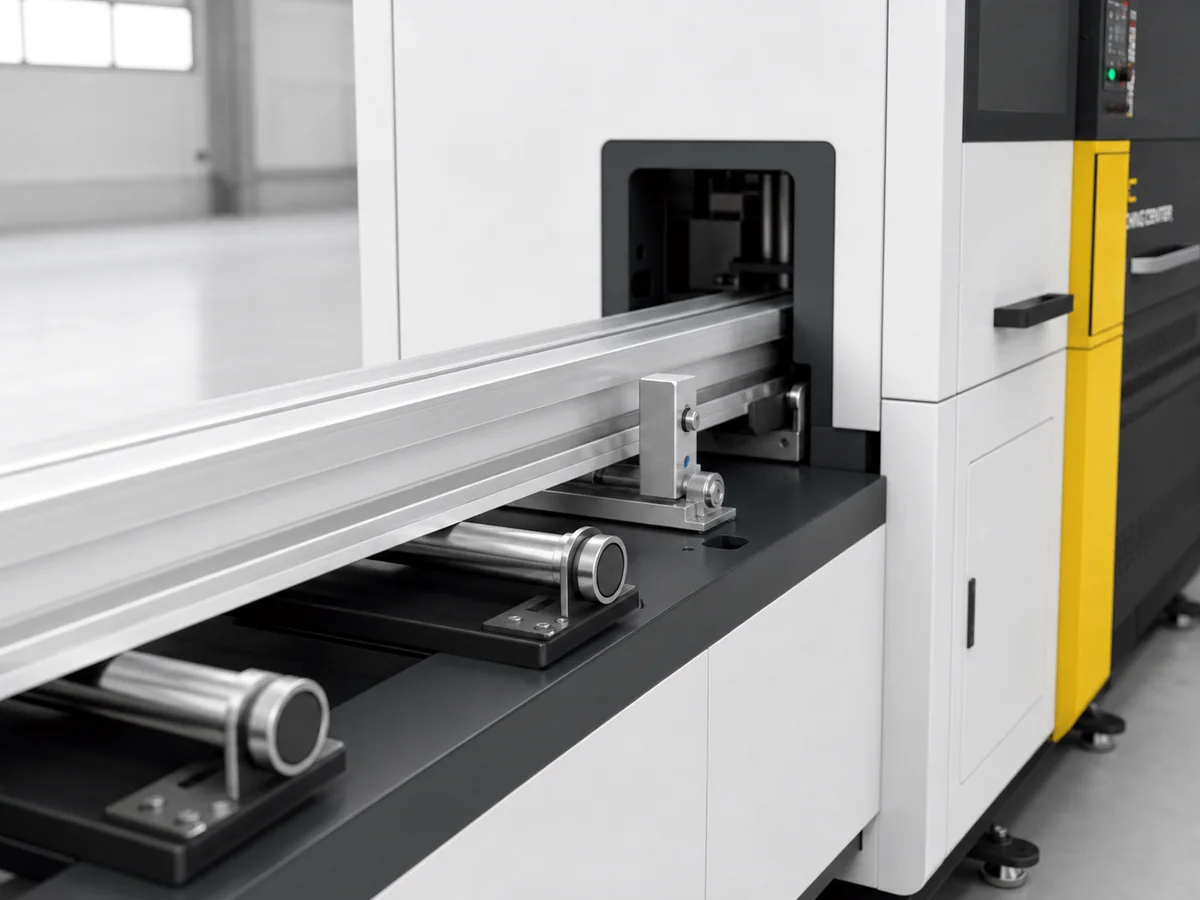
The infeed rollers are easy to see; the moving carriage guide may be hidden behind a cover. That difference matters when a maintenance request says “grease the feed rail.” Aluminum saw linear guide lubrication starts by identifying the actual motion component and its approved service point. A shiny stock-support roller, an adjustable side fence and a recirculating linear guide do different jobs. Putting grease on the visible one does not service the hidden one.
Trace the moving axis before naming a lubricant
Ask the machine supplier for the feed-axis assembly drawing or service view for the installed configuration. Mark the moving carriage, rail, guide blocks, protective covers and every specified lubrication port. If the machine uses another motion arrangement, use that arrangement’s instructions instead. The model name or an exterior photograph cannot establish that a particular linear guide is fitted.
Follow the motion path through a complete feed stroke without reaching inside a live machine. Note which part carries the stock and which part constrains the carriage. This separates stock guidance from the precision motion elements that could need grease. A maintenance technician should then check the machine’s isolation procedure before opening a guard or cover; the operating video below is not a service instruction.
Aluminum saw linear guide lubrication: whose interval applies?
THK’s LM Guide technical material explains that lubrication depends on operating conditions, environment and mounting orientation. It advises normally replenishing through the specified nipple or hole with the same grease type; mixing greases can change consistency and performance. Its approximate 100 km or three-to-six-month reference is a guide-maker example, not a service interval for a Jiurun saw. The final amount and interval must come from the actual installed guide and machine supplier.
For aluminum saw linear guide lubrication, a purchasing team should not order “general-purpose grease” from a photograph. Ask for the guide maker and designation, the approved product, the amount per block or port, the access method and the schedule basis. If the machine is vertical, angled or has remote lines, confirm how lubricant reaches each block. THK cautions that orientation can affect distribution; a different guide maker may specify a different method.
Keep chips out of the service decision
Before replenishment, inspect the cover, seals and exposed travel area under the machine’s approved isolation procedure. Aluminum chips packed near a block, a damaged wiper, an empty automatic reservoir and an inaccessible nipple are different findings. Record each one rather than calling all of them “dry rails.” Clean only by the supplier’s approved method; forcing debris under a seal while adding grease defeats the purpose of the service.
Match the grease container to the specified port and record its identity. Do not substitute MQL cutting fluid for guide grease: the cutting-zone fluid and the axis lubricant serve different systems. Our earlier aluminum saw lubrication scope guide separates those equipment boundaries. If the existing lubricant is unknown or a change is proposed, obtain a documented compatibility or changeover instruction before mixing products.
Release the axis with motion evidence, then a cut
After the approved service work and guard restoration, compare the axis with its pre-service baseline. Record the carriage’s motion over its usable travel, any abnormal noise or resistance, and the control’s position or fault response. THK notes that fresh grease can temporarily raise slide resistance; that possibility is a reason to follow the specified warm-up and observation procedure, not to override a fault. A sudden bind, leak or repeated alarm needs diagnosis before production release.
Then run a representative feed-and-cut sequence and inspect finished pieces against the agreed drawing and measurement method. A stable cut length after greasing does not prove the guide was the cause of an earlier problem; it only supports the specific release trial. If the first piece after a direction change differs from later pieces, our feed-reversal article explains how to separate commanded motion, stock travel and measured output.
What the equipment video can show
The following video is from Jiurun Machinery’s own channel. It shows an automatic aluminum saw’s feed and cutting area. It does not expose the guide blocks, specify a lubricant, document maintenance, or prove the result of the procedure described here.
Ask for the service boundary, not a grease brand guess
For aluminum saw linear guide lubrication on an existing machine, send the supplier a photo of the machine nameplate, the feed-axis service drawing if available, the observed symptom and the current lubrication record. Request the installed guide designation, service access, approved lubricant and amount, safe sequence, and post-service motion test. For a new saw quotation, ask which feed components require periodic lubrication and which documents and access tools are included at handover. That makes the future maintenance task measurable without assuming that every machine shares the same rail.
Contact JiurunCut with the profile drawing, planned cut range and feed-axis questions. We can discuss the saw configuration and the evidence needed for your application; the final service instruction must match the machine actually supplied.