
Aluminum saw blade speed needs a named quantity and a unit. Rotational speed describes how many revolutions the blade makes in a minute. Peripheral cutting speed describes how fast a point on its cutting circumference travels. Blade diameter connects the two quantities, so the same RPM does not give the same rim speed for every diameter.
For a machine quotation, separate the stated blade rotation, the proposed cutting condition and the tool’s permitted limit. Four checks help buyers read these entries and request a review for the actual blade and aluminum section. The numerical examples below explain the arithmetic; they are not machine settings.
Name the quantity beside every value
- Blade rotational speed: revolutions per minute, or RPM.
- Peripheral cutting speed: a linear speed, with its units stated.
- Feed speed and blade rotation: separate entries in the process description.
On this page
Check 1: identify the quantity for aluminum saw blade speed
When a quotation says “speed,” ask what is moving. Is the entry for the blade, a motor, a material-feeding movement or another axis? Retain the supplier’s meaning and units in the comparison sheet.
A motor nameplate describes its own motor information. Ask the machine supplier how the quoted blade rotation relates to the specified configuration. Do not treat an unrelated motor value or displayed axis movement as a measured blade RPM.
Distinguish a listed machine value from an adjustable range and from a proposed operating condition. Ask which applies to the actual quotation. A controller image alone does not confirm the speed options supplied with the machine.
Also ask which statement is a tool limit and which is an application recommendation. Those entries need their documented purpose beside them. A numerical comparison without that context can make unlike statements appear equivalent.
Check 2: connect blade diameter and units
For a rotating circular tool, the peripheral speed is its circumference multiplied by its revolutions over time. With diameter D in millimetres and blade rotation n in RPM, the result in metres per second is:
Peripheral speed v = π × D × n ÷ 60,000.
The diameter conversion contributes a factor of 1,000, and converting minutes to seconds contributes a factor of 60. Keep those conversions with the formula. Using the same expression with a diameter in metres would require a different conversion factor.
LEUCO’s tool document, section 5.1, presents this cutting-speed relationship with millimetres, RPM and metres per second. The document concerns Rauvisio Cube panels. Only the general unit relationship is used here; its panel tooling and process recommendations are not aluminum cutting recommendations.
If a supplier gives the peripheral speed in metres per minute, divide that value by 60 to express it in metres per second. A value shown as m/min cannot be compared directly with the same number shown as m/s.
A worked arithmetic comparison
The following diameters and rotations are fictional arithmetic inputs. They do not identify an available machine, an approved blade or a suitable aluminum cutting condition. No result is a recommendation to install a different blade or change a machine speed.
| Example | Diameter and rotation | Calculated rim speed |
|---|---|---|
| A | 300 mm; 1,000 RPM | 15.71 m/s |
| B | 600 mm; 1,000 RPM | 31.42 m/s |
| C | 300 mm; 2,000 RPM | 31.42 m/s |
For A, the calculation is π × 300 × 1,000 ÷ 60,000, rounded to 15.71 m/s. B doubles the diameter while keeping the rotation unchanged, so its calculated peripheral speed doubles. C instead doubles the rotation at the original diameter.
B and C have equal calculated rim speeds but different diameters and rotations. That mathematical equality does not establish equal cutting quality, tool compatibility or machine capacity. The actual process still needs its own approved tool and setup review.
For a unit comparison, A is approximately 942.48 m/min before division by 60. State the unit every time the result is transferred to another document. Rounding a calculation does not create a permitted operating range.
Check 3: confirm the documented machine and tool limits
Identify the exact blade and the proposed machine configuration. Request the applicable machine instructions and tool information, including the permitted rotation and intended material application. Have the responsible suppliers confirm the proposed combination through their approved process.
A blade’s maximum permitted rotation is a limit, not a production target. A calculated rim speed only describes the arithmetic relationship for the selected inputs. Neither entry, by itself, selects a suitable aluminum cutting condition.
Keep blade diameter, bore, body, cutting width and other specified interfaces in the review. The blade-size quotation guide explains why the complete tool identity matters. A speed calculation does not authorize an alternative diameter or mounting arrangement.
Retain the actual supplier’s operating requirements. This article does not prescribe a speed, feed, lubrication method or blade replacement procedure. Any machine adjustment belongs within the applicable instructions and authorized operating process.
Check 4: review the actual cutting condition and result
Provide the aluminum alloy and temper, profile drawing, wall geometry, stock condition and finished-part requirements. Ask the supplier to define the tooling and process scope for that material. A rotation stated for a different tool or workpiece is not an approved transfer.
Record feed information separately, naming the relevant movement and units. Blade rotation, peripheral speed and feed describe different quantities. The tooth-count review connects the identified blade with its geometry and application information without turning one field into a complete selection rule.
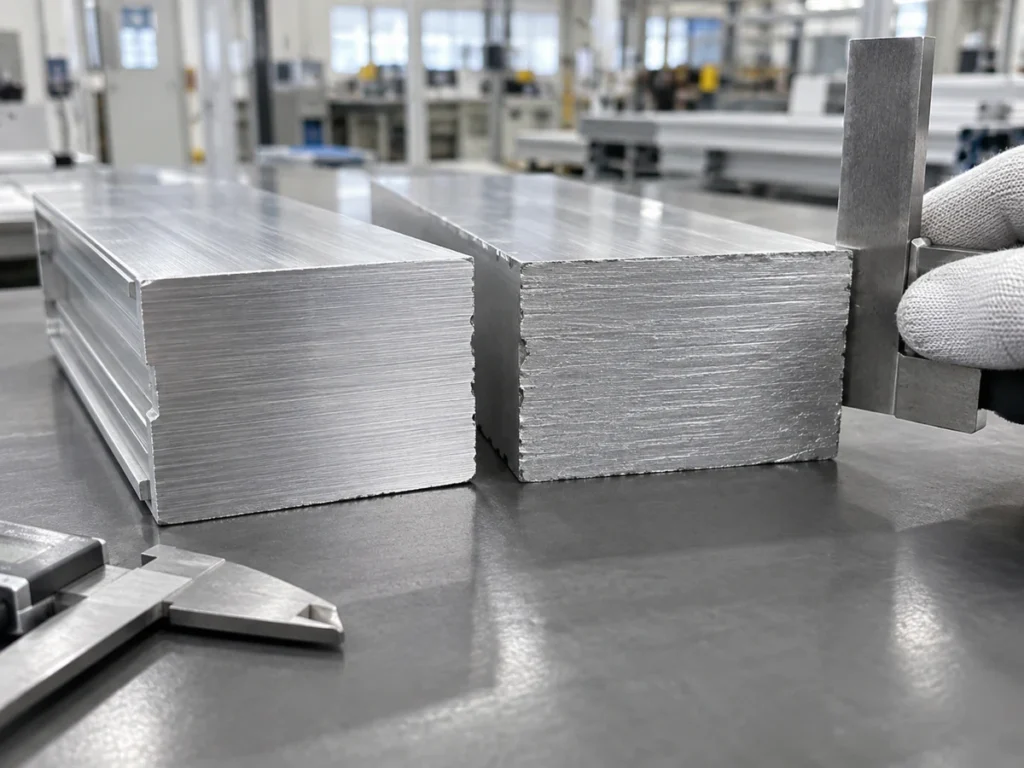
For a representative evaluation, retain the stock, blade and setup identities with the inspected results. Use the agreed length, angle, end-face, edge and handling checks. The sample-cutting checklist can help define what the demonstration needs to show.
Keep the result and its scope visible. A successful read of a speed display or a short cutting clip does not establish a batch acceptance result. Ask for the actual trial records relevant to the proposed material and requirements.
A clearer quotation brief
Replace an ambiguous “high speed” statement with entries the buyer and supplier can review together. Include the following information without filling unresolved values from unrelated examples:
- Machine: quoted configuration and applicable blade-speed description.
- Blade: exact identity, diameter, interfaces and supplied application information.
- Quantities: rotational speed, peripheral speed and feed, each with its meaning and unit.
- Review: permitted combination, representative stock and agreed result checks.
For a JiurunCut inquiry, send the actual section drawing and cutting requirements. Ask which speed statements and tooling apply to the proposed configuration, and how they will be confirmed. No particular JiurunCut model’s RPM or variable-speed capability is asserted here.
Buyer questions about saw blade speed
Does equal RPM give equal peripheral speed?
Only when the relevant cutting diameter is also equal. Peripheral speed depends on both diameter and rotational speed, with the units handled consistently.
Does equal peripheral speed mean equal cutting performance?
No. It is one calculated quantity. The actual tool, material, machine and approved process determine what must be reviewed in the cutting evaluation.
Can the example values be used as machine settings?
No. They are arithmetic inputs. Use the actual machine and tool instructions and the responsible supplier’s approved application review.