
Aluminum extrusion die types describe the tooling used to form a profile at an extrusion press. Buyers often encounter solid, semi-hollow and hollow terminology, but a profile category is not a complete die specification. The extruder needs the controlled cross-section and production requirements to define the tooling.
Three distinctions make the discussion easier: the profile shape versus the die arrangement, a void in the profile versus an aperture in the die, and an extrusion die versus a saw fixture. Understanding those differences helps you request a clearer quotation and pass the right information to a cutting supplier.
Start with the cross-section
- Show enclosed spaces, open gaps and functional surfaces on the drawing.
- Ask the extruder to confirm shape classification and die scope.
- Keep extrusion tooling separate from the later cutting fixture.
On this page
Aluminum extrusion die types begin with the profile drawing
The Aluminum Extruders Council’s design tips describe solid, hollow and semi-hollow profile categories. A hollow profile fully encloses a void. A partially enclosed space needs more care: an open shape is not automatically semi-hollow, and the extruder can help resolve the classification.
The drawing should show the entire cross-section rather than a cropped detail. Include dimensions for openings and internal features as well as the outside envelope. A three-dimensional view can help explain function, but it does not replace that controlled section drawing.
| Visible shape feature | Useful first question |
|---|---|
| No enclosed space | Does the complete section have a semi-hollow condition? |
| Partially enclosed space | How does the extruder classify the opening and supported tongue? |
| Fully enclosed space | Which hollow tooling arrangement is proposed? |
Solid profiles can include more than plain bars
A round bar is an easy visual example of a solid section. The category can also include shaped sections and projections. “Solid” does not mean every profile must be a simple rectangle or that every tool will have one aperture.
AEC’s dies and tooling guide explains that a solid die can have multiple apertures for separate extrusions. Ask the extruder to confirm the arrangement for your profile.
For procurement, use the supplier’s confirmed classification alongside the drawing reference. If an offer simply says “solid die,” ask which profile revision it covers and what tooling is included. Do not infer those details from the label.
An open channel needs a classification check
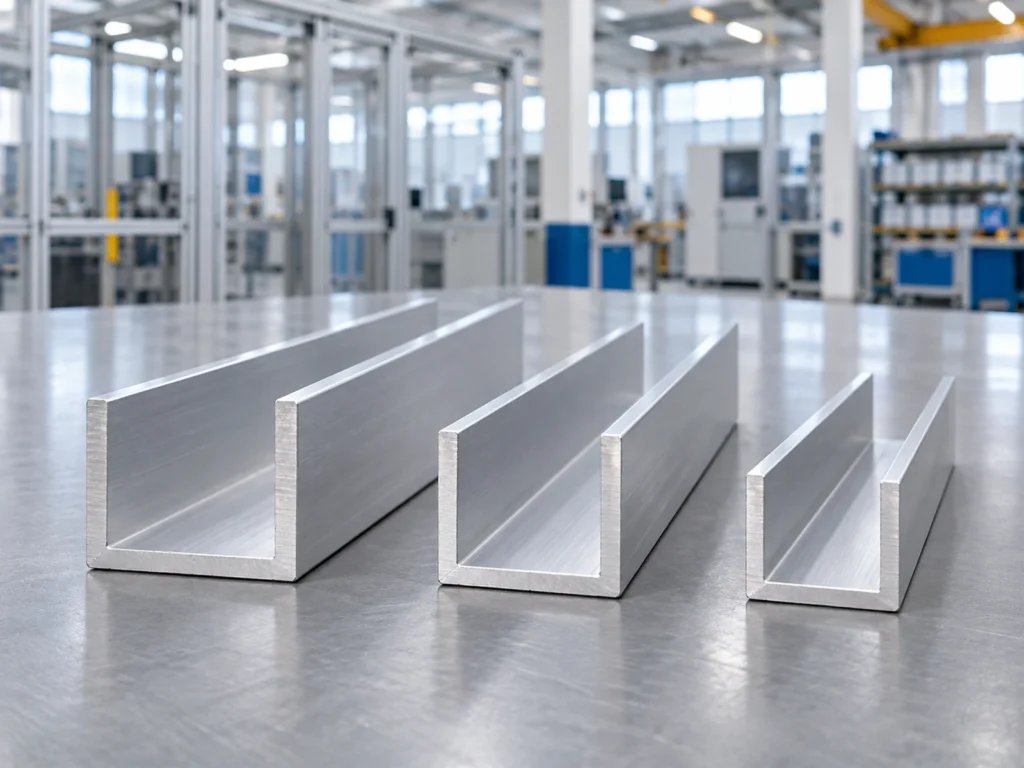
A semi-hollow question concerns a partly enclosed space and the tooling that supports its internal shape. AEC relates this condition to the size of that space compared with the gap connecting the die tongue to the surrounding tool.
Looking only for an open side is insufficient. A wide opening and a narrow opening can create different questions for the extruder. Keep the exact gap and surrounding geometry in the drawing rather than identifying the profile from a generic photograph.
If the supplier proposes widening a gap or changing an internal feature, ask the product designer to review the function first. A cover, fastener or mating part may depend on that feature. Approve the revised profile before asking the cutting supplier to work from it.
Hollow profiles do not identify one universal tool
AEC’s tooling guide lists bridge, porthole and spider arrangements among hollow die forms. It says the selection depends on the profile, the press and container, and production requirements. A closed void in the product is therefore a starting point for discussion, not a complete tooling choice.
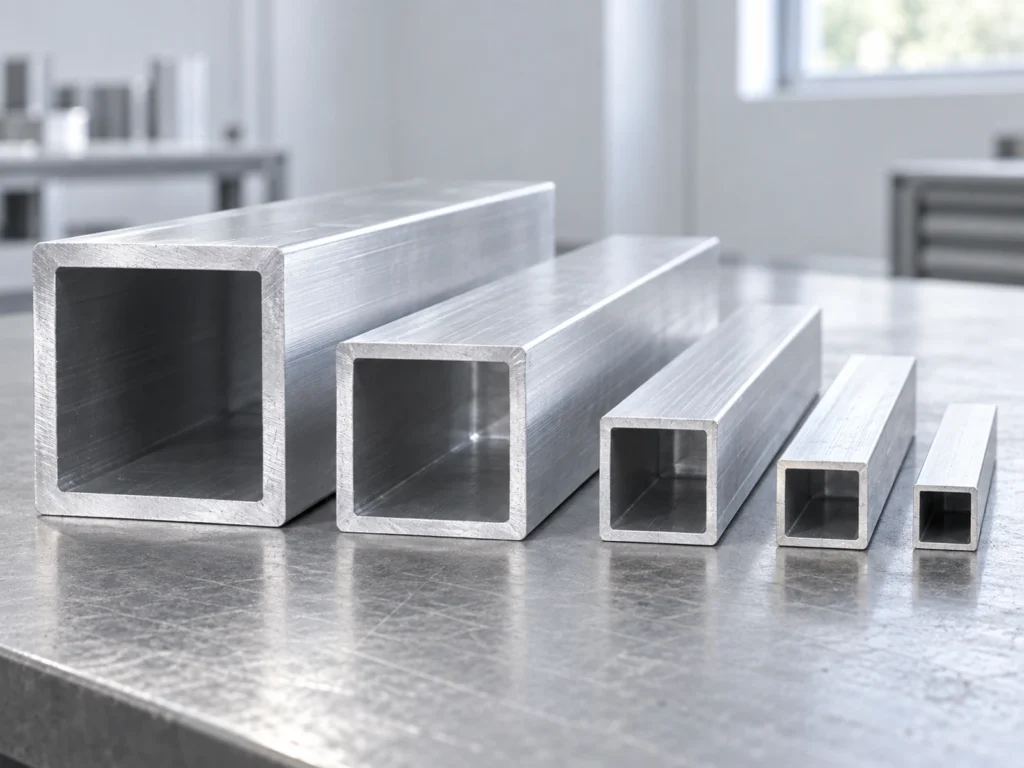
A square tube with one enclosed opening can illustrate the profile category. It cannot show which tool produced it, how material moved through that tool or which process route the supplier used. Obtain those details from the supplier’s production information when the application requires them.
Our seamless versus structural tube guide explains why a tube’s visible outside shape is not proof of its manufacturing route. Carry any approved route requirement into the material order as well as the tooling discussion.
Three distinctions that keep aluminum extrusion die types clear
1. Profile category and die arrangement are different descriptions
The profile category describes the cross-section. The die arrangement describes how the supplier will form it. Record both when comparing offers, but let the extruder define the proposed tool against the approved drawing.
Hydro’s profile overview describes dies with different shape combinations and single or multiple openings. This supports checking the proposed arrangement rather than assuming a one-to-one relationship between a familiar shape name and a complete tool.
2. A profile void and a die aperture are not the same count
A void is an enclosed empty region in the resulting cross-section. An aperture here means an opening used to produce a separate profile. If a quote uses “two cavities,” ask the supplier to draw or define what the word refers to.
Do not convert that phrase into a part-output claim. The order still needs an agreed quantity of accepted profiles or cut pieces, with its own material and acceptance requirements.
3. An extrusion die and a cutting fixture do different jobs
The extrusion die forms the long profile. The cutting fixture locates and holds that profile for sawing. Paying for one does not explain the design or supplied scope of the other.
Send the finished stock section and its functional surfaces to the cutting supplier. Our clamping review guide helps organize that later discussion. Keep the tooling references distinct so a purchasing line cannot be mistaken for a saw fixture.
Five questions for an extrusion tooling quotation
- Drawing: Which complete profile revision and material requirement does the offer cover?
- Arrangement: What does the supplier mean by solid, semi-hollow, hollow or cavity count?
- Included tools: Does the price identify the die and any supporting tooling?
- Approval: What sample review and drawing approval must occur before the production order?
- Records: How will the approved tool reference connect to later profile orders?
AEC explains that extrusion tooling can include supporting tools as well as the die. Ask for the scope to be itemized. For order quantities, use our custom extrusion MOQ guide to separate the tooling discussion from the profile order requirement.
A fictional mix-up: one product void, two die apertures
Imagine profile X20 is a square tube with one enclosed void. A supplier proposes an arrangement producing two separate X20 extrusions. The buyer’s spreadsheet shortens the description to “two-cavity tube.”
That label could make another supplier interpret X20 as a profile with two enclosed voids. The clearer record keeps the drawing unchanged and states separately that the proposed die has two profile-producing apertures. This fictional example explains terminology; it is not an actual tool design or production-rate calculation.
Buyer questions
Can a photograph establish aluminum extrusion die types?
A photograph may show visible shape features. It does not establish the complete die design. Request the controlled profile drawing and the extruder’s confirmed tooling description.
Does “hollow die” mean that every hollow profile is interchangeable?
No. Compare the exact section, material, manufacturing requirements and acceptance scope. The category does not make different profiles substitutes for each other.
What does JiurunCut need for a cutting review?
Send JiurunCut the approved stock cross-section, cut-part drawing, quantity and handling requirements. Include the actual material supply requirements so the cutting discussion starts from the profile you intend to use.