
An aluminum damper frame can look simple in a bill of materials: four cut members around a moving blade assembly. For a saw buyer, however, “cut the frame” is not a complete request. The released extrusion, the corner connection, and the features installed after sawing determine what the cut shop must deliver. This guide gives an OEM buyer seven checks for an aluminum damper frame cutting RFQ. It covers straight frame-member blanks only; damper design, assembly, airflow and leakage qualification remain with the product owner.
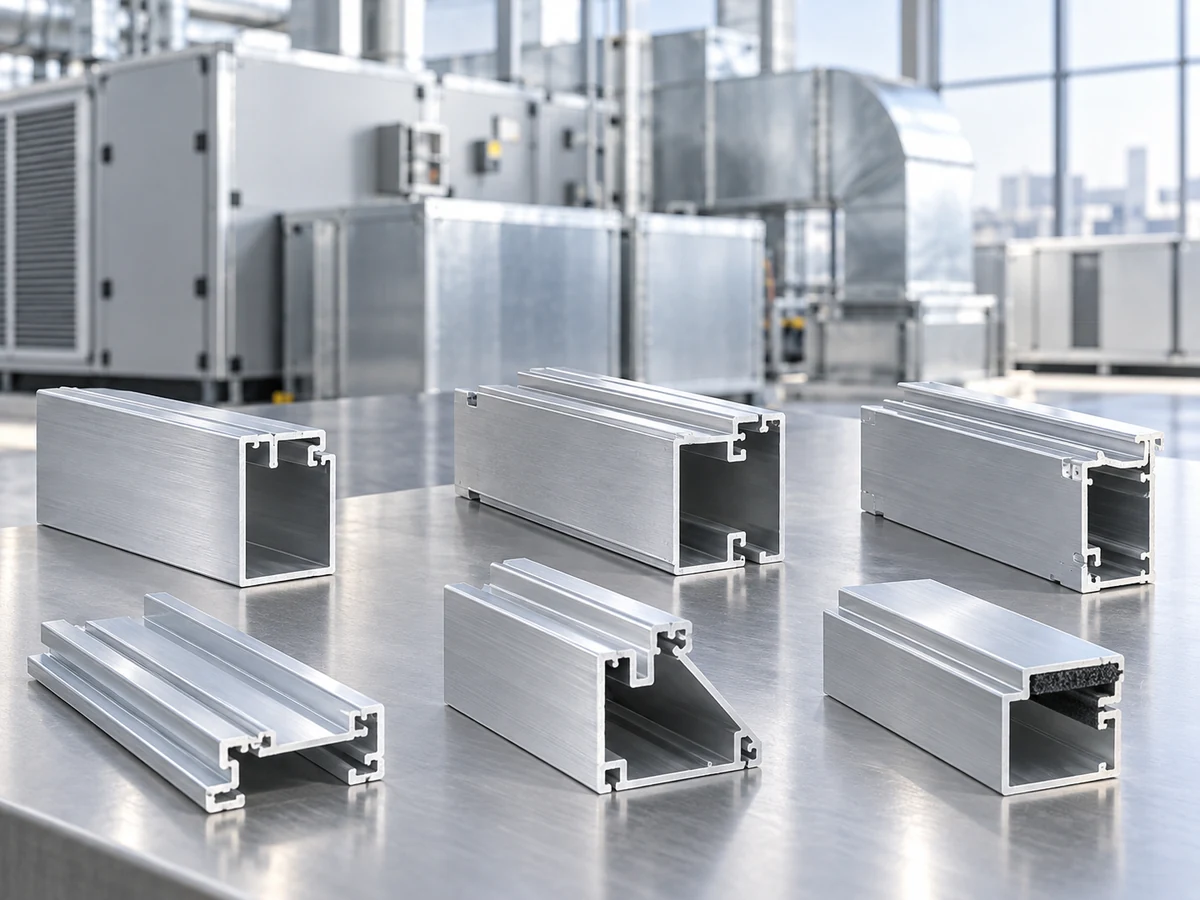
1. Name the exact member and the accepted supply stage
Start with a controlled drawing and revision for each frame rail or jamb. State whether the supplier receives approved extrusion stock, a prefinished member, or a purchased frame kit. A damper may contain aluminum blades, frame members, seals, bearings, shafts and linkage. Those are different procurement objects. For example, Greenheck’s VCD-43 product description identifies an extruded aluminum airfoil blade and frame with blade and jamb seals. That product example shows why a frame-cutting quote should not silently include blade manufacture, seal installation or finished-damper performance.
Ask the buyer’s engineer to mark the exact frame section in the released profile drawing. Record alloy and temper only from the approved material specification; do not infer them from a photo or a general HVAC label. Specify the receiving condition, protective film if applicable, and who owns any finishing or machining after the saw.
2. Build the cut list from the assembly drawing
List each member by part number, revision, extrusion section, finished blank length, quantity per damper, and intended receiver. Distinguish top and bottom rails from side jambs if their ends, orientations or later operations differ. Mark the reference face and the end from which the length is measured. A cut list with only an overall damper width and height leaves the supplier to guess the corner allowance and whether dimensions describe an outside envelope or an individual blank.
When multiple damper sizes share a section, show the complete size family and the actual order mix. A long stock bar, a short rail and a small jamb may change handling and first-off inspection even though the profile is nominally the same. Use representative pieces from that mix in a witnessed trial before agreeing a production rate.
3. Define the corner and end condition for aluminum damper frame cutting
The drawing must say whether the blank end is square, mitered, notched later, or intentionally left with machining allowance. Include the accepted length datum and any end-face, burr or edge condition needed by the downstream joint. Do not ask the saw supplier to invent a corner detail. The frame assembler must identify the actual connector, fastener, weld or other approved joint route, and the cutting quote must state where the saw’s work ends.
4. Test support and contact on the released extrusion
Thin walls, open channels and projecting lips can react differently to stock support and clamp contact. Give the saw supplier a sample of the actual released section and identify faces that may be supported, clamped or marked. Request a trial that includes the longest and shortest relevant blanks, the planned feed orientation, and the accepted face condition. Record what the trial shows instead of claiming a generic machine configuration will suit every damper frame.
The trial should also show how the operator identifies the correct stock before cutting and prevents another profile family from entering the same job. If a surface finish is applied before cutting, agree whether contact marks and exposed cut faces are acceptable at the receiving stage. If finishing follows cutting, document that handoff instead of attributing finish quality to the saw.
5. Protect downstream seal, shaft and linkage interfaces
A cut frame member is only one input to the finished damper. Ruskin’s CD450 product page illustrates a system with airfoil blades, jamb seals and linkage-related options. These examples do not define another OEM’s dimensions. Ask the damper design owner which rail ends or faces locate later seals, bearings, axles or linkage, then mark only the cut-stage requirements that follow from the released drawing. Hole patterns, seal grooves and installed hardware should be quoted separately if they are outside the saw operation.
Do not convert an acceptable cut length into a claim of leakage class, airflow performance or completed-damper fit. Those outcomes require their own assembly and product verification. The saw-trial record should name the blank, drawing revision and measured cut criteria, with a clear handoff to subsequent work.
6. Agree first-off inspection and bundle identity
For each job change, identify a first-off sample and the person who releases the remaining batch. The inspection plan can include length from the specified datum, end orientation, visible burr or edge condition, and the surfaces most likely to be damaged in handling. Use the drawing’s actual tolerances and inspection method; a generic tolerance invented for an article is no substitute. Keep accepted pieces, rework holds and offcuts distinguishable.
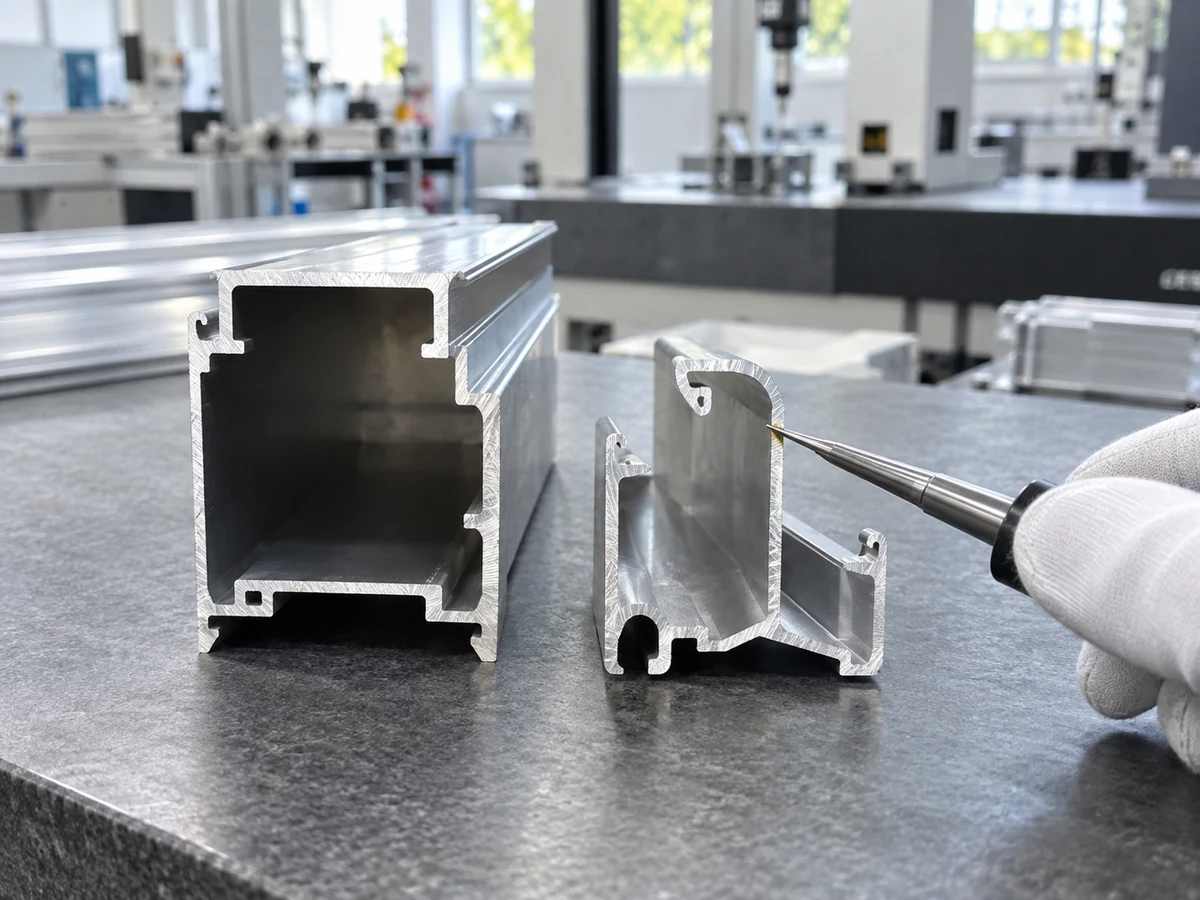
Label each released bundle with the part and revision, material lot or batch reference, quantity, and destination assembly order as required by the buyer’s traceability plan. Our separate saw-output traceability guide explains the general job-to-bundle handoff. For a damper frame RFQ, the specific question is whether a top rail and a similar-looking jamb can be mixed without anyone noticing before assembly.
7. Compare complete, accepted output in the RFQ
Ask each supplier to quote the same released mix and the same accepted blank stage. Define who supplies the extrusion and blade, who prepares a fixture, and whether loading, unloading, inspection, segregation, scrap and packaging are included. State the expected shift pattern and job-change frequency. Compare the elapsed work for a complete accepted batch, including first-off checks and changes between lengths, rather than a single idealized cut cycle.
| RFQ field | Buyer-supplied decision | Evidence to request |
|---|---|---|
| Released member | Part, revision, section and input condition | Drawing-linked sample identification |
| Cut geometry | Length datum, end orientation and corner allowance | First-off cut and recorded measurements |
| Handling | Permitted support/contact faces and finish condition | Trial observations on actual stock |
| Output | Bundle identity, quantity and receiving stage | Accepted batch and hold/offcut separation |
| Scope | Included labor, fixtures, inspection and downstream exclusions | Comparable complete-batch quote |
Equipment video: a general saw demonstration
The Jiurun Machinery video below shows an aluminum-saw equipment example. It helps a buyer visualize stock feeding and a guarded cutting station. It does not establish the damper section, model configuration, customer job, trial outcome, accepted length or finished-damper performance discussed here.
Before you request a price
Send the released section drawing, member cut list, expected job mix, actual material sample, permitted contact faces, first-off criteria and receiving-stage definition together. Ask the supplier to identify any assumption or missing decision in writing. That package gives you a way to compare saw proposals without confusing a cut blank with a qualified damper. To discuss an actual aluminum-profile saw trial with Jiurun, contact the team with your released drawings and sample details.