
Aluminum saw setup cuts create a small but consequential buying question: where do the first pieces go while a new profile, blade, fixture or program is being proved? A supplier may demonstrate a good finished part, yet the trial pieces, adjustment cuts and accepted production pieces can leave the machine through the same outlet. If the quotation describes only cutting capacity, the buyer still has to design the release boundary. Ask the supplier to show that boundary during the trial, and assign the people, containers and records that keep unapproved pieces out of a shipped batch.
This guide is about the disposition of setup pieces when buying or integrating an aluminum saw. It does not replace dimensional inspection, a first-article procedure or a customer’s drawing. It helps a buyer turn those requirements into a physical, testable production handoff.
Aluminum saw setup cuts: define the boundary before comparing saws
Write down the exact event that starts a new setup: a different part number, extrusion section, angle, cut length, blade, clamping arrangement or approved program revision. The list depends on your work, not a generic machine feature. For each event, identify what the saw might produce before the process is released. That may include a short positioning cut, a trim end, a first full-length sample and pieces made during adjustments. Do not assume that every piece cut before approval is automatically scrap; a measured sample may be retained as evidence. Equally, do not count an unapproved sample as saleable output merely because its length happens to pass one check.
Separate three decisions in the RFQ: why a piece was cut, what checks it needs and who may release it. This prevents an operator, quality reviewer and purchasing team from using the word “sample” for different things. If customer requirements already define the release rule, copy that rule into the trial plan rather than inventing a machine-specific tolerance.
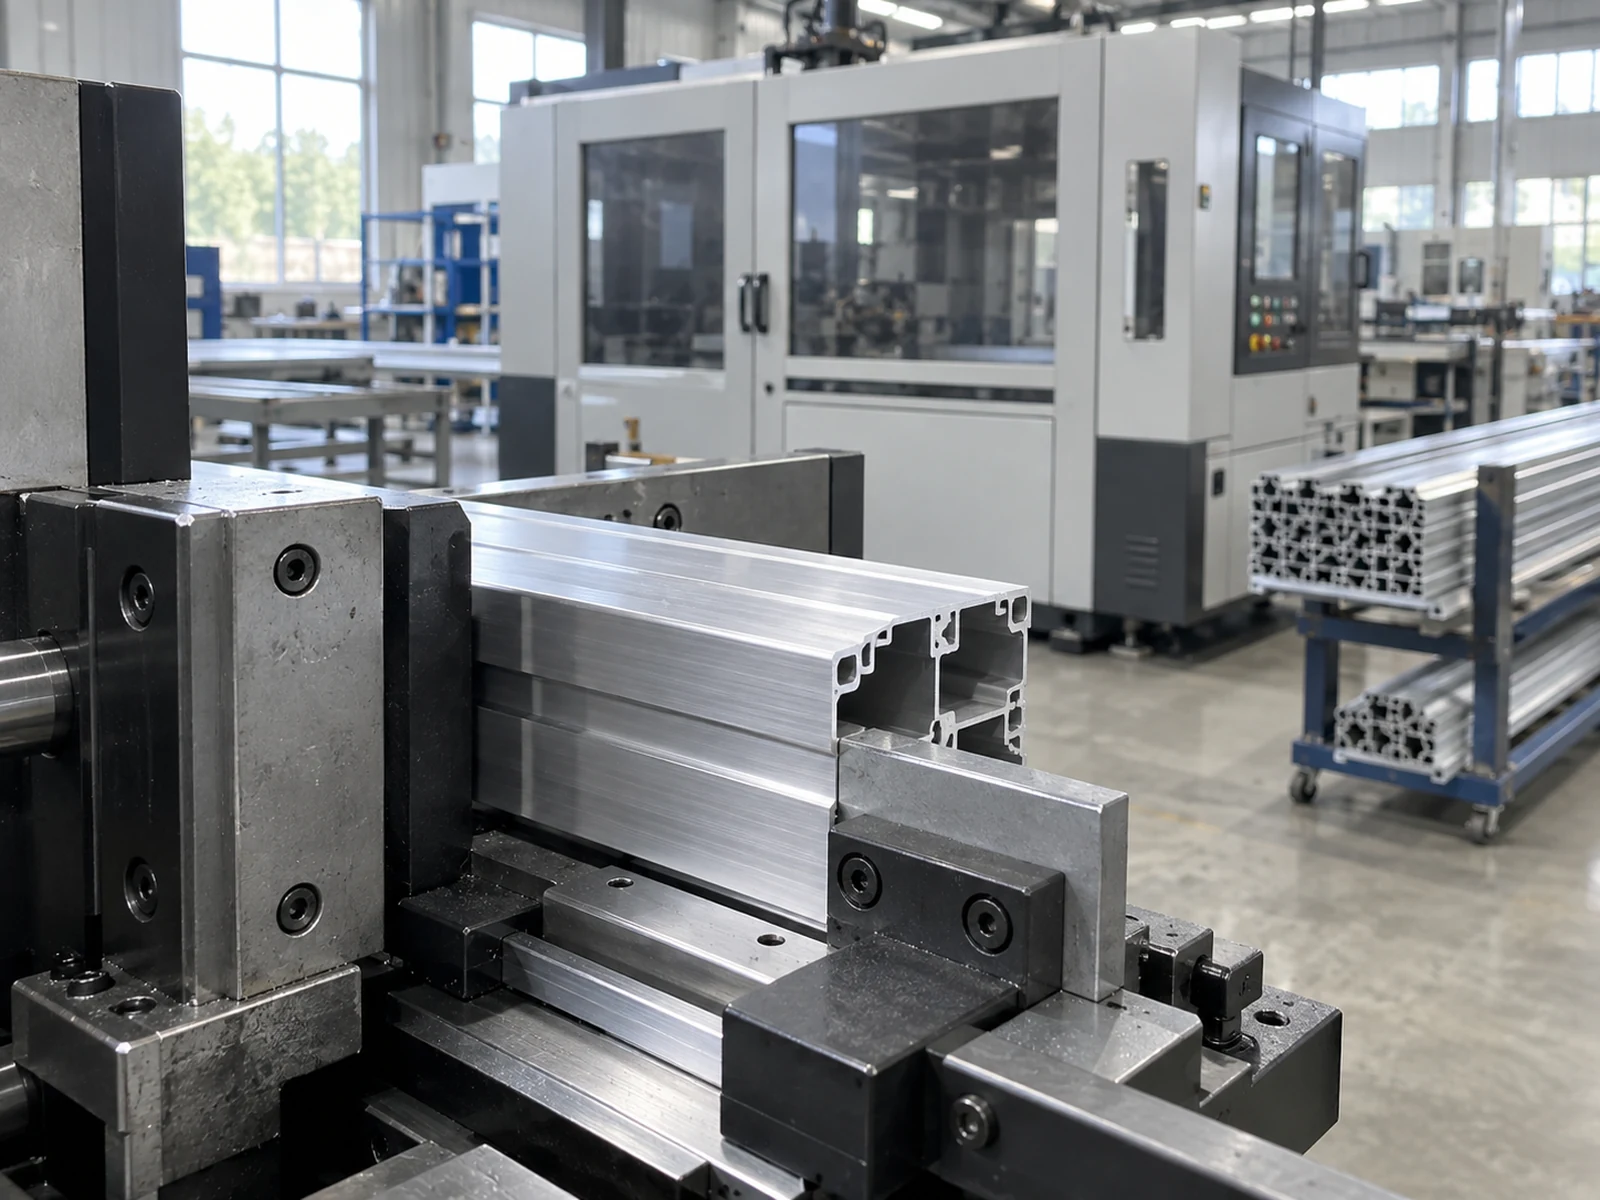
Give each trial piece a physical route
For aluminum saw setup cuts, a written instruction alone will not prevent mixing if every piece lands in one common bin. Walk the route from blade to outfeed, inspection bench and packing point. Where will the first piece wait? Where will a rejected adjustment cut go? Where will an accepted part go after release? Decide whether the operator can reach each destination without carrying a piece across a live feed path. Review this with the actual shortest and longest pieces in the buyer’s part mix; a chute or tray that works for one length may change the handling task for another.
Mark trial and accepted locations so their status remains legible when the operator changes, the bin moves or production pauses. A tag can carry job or part identity, setup reason, time, current status and the person responsible for the next decision. A color by itself is weak evidence if colors are reused or a label becomes detached. If a trial piece is deliberately retained for later measurement, specify where it stays and how it links back to the corresponding job. If it is to be discarded, specify the authorized disposal route so it cannot return as an unrecorded remnant.
Measure, decide and release the first production pieces
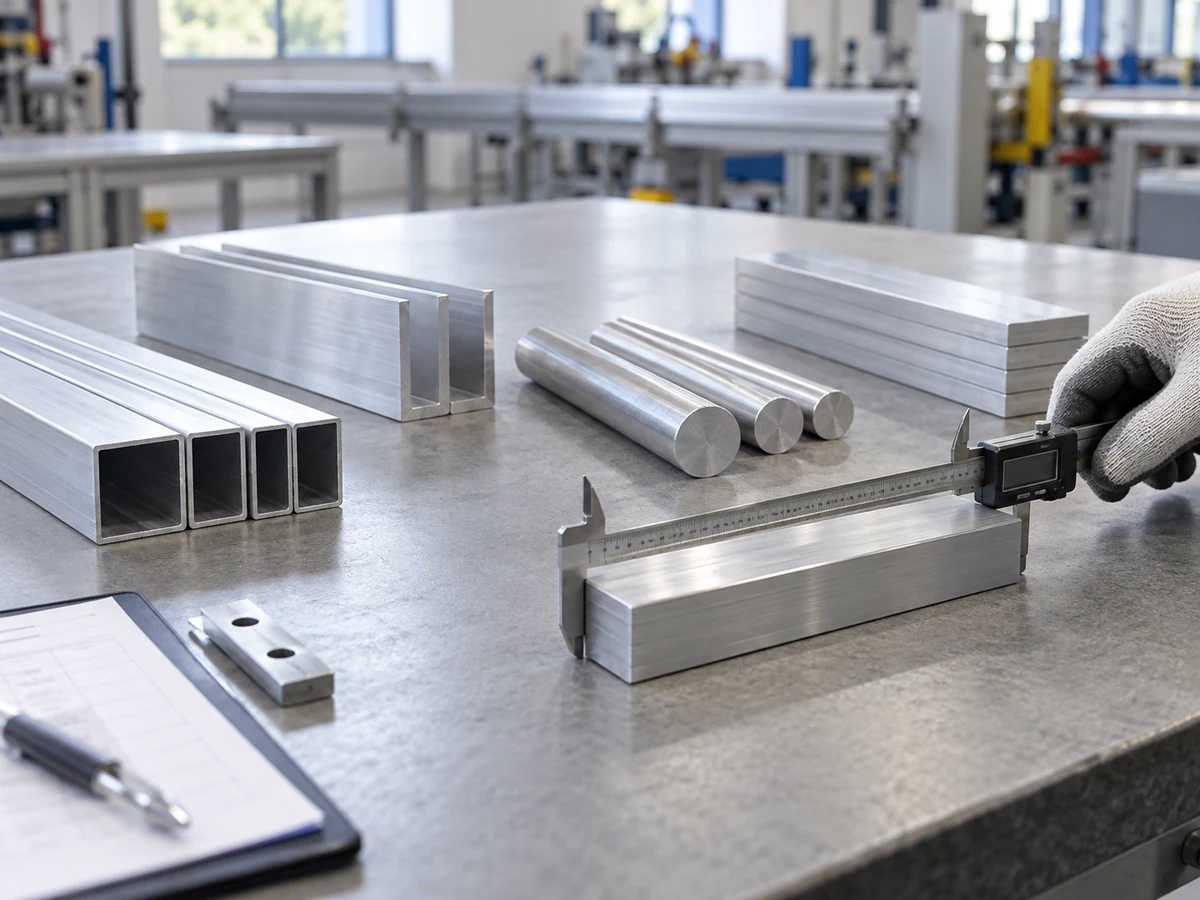
The buyer should define the applicable drawing revision, datum, measurement method and acceptance authority before the saw trial. A first piece may need length and cut-end checks; an angled part may need a different check against its mating component. Do not let a nominal machine setting stand in for a measured part. Record which physical sample was checked, what result was obtained and whether the decision releases the process, the sample itself, or both. Those are different approvals.
Consider a job in which an operator cuts one positioning end, then a full-length sample, adjusts the stop and cuts another sample. The release record should identify all three pieces and say what happened to each. It should also define which subsequent piece begins the accepted production count. A buyer can ask the supplier to demonstrate the sequence with the buyer’s approved drawing and a representative profile. No universal number of samples or guaranteed measurement result is implied here; the correct sampling plan depends on the released part and customer requirement.
Keep the accepted count separate from saw strokes
A saw counter can report cycles, pieces or programmed quantities depending on the system. Ask exactly what its number includes: trim cuts, test pieces, rejected parts, recuts and saleable parts may be counted differently. For a purchase comparison, define the output number that matters to your plant: released parts of the correct job, reconciled with the physical container and inspection record. If the supplier proposes automated count transfer, prove the mapping during a setup change rather than accepting a screen total as a shipment total.
This boundary also affects yield and cost. A quote that assumes every cut is saleable may make a fast changeover look cheaper than it is. Request a trial sheet that distinguishes stock consumed, setup pieces retained, scrap, rework and released pieces. Use the actual profile, order mix and acceptance criteria for that comparison. Do not convert a claimed feed positioning figure into finished-part accuracy or use a promotional cutting rate as the accepted-output rate.
Test the boundary at a real changeover
A useful acceptance demonstration changes one job condition that normally creates setup pieces. Stop the first job, identify the final accepted piece, load the next approved job and cut its trial sequence. Ask the operator to show where each piece lands and how it is identified before anyone knows whether it passes inspection. Have the reviewer make the release decision using the agreed method. Then reconcile the accepted counter, trial container, reject container and next job’s packing location. The test should fail visibly if a piece has no clear status or if a later operator cannot reconstruct the decision.
Repeat the discussion for an interrupted run. If the machine is stopped for an alarm, blade change or program correction, who decides whether a fresh setup check is needed? The answer belongs in the buyer’s controlled process and the supplier’s handover, not in an assumed feature list. For a broader stock-to-release record, see the aluminum saw job traveler. For the inspection evidence itself, see first article inspection records.

Put these deliverables in the aluminum saw RFQ
- Part mix and trigger list: representative profile sections, lengths, angles, quantities and the changes that require a new setup decision.
- Piece-status map: where trim, trial, held, rejected and released pieces go from the cut zone to packing.
- Release rule: applicable drawing revision, inspection method, decision authority and the point at which accepted production counting starts.
- Counter definition: whether the quoted output and machine display mean strokes, cut pieces or released parts.
- Trial evidence: photos or a witnessed walkthrough of the physical routes, sample identity, measurement record and count reconciliation.
- Handover scope: the bins, labels, instructions, training and data fields supplied with the machine versus those provided by the buyer.
Ask suppliers to quote the same scope. A saw may cut the profile correctly while the buyer still has to provide the downstream status control. That can be a valid purchase, but the responsibility should be explicit before acceptance. ISO’s guidance on documented information emphasizes retaining evidence where output identification, production changes and nonconforming-output decisions matter; apply the requirements relevant to your own quality system rather than treating this article as a certification claim. Read the ISO guidance on documented information.
Equipment footage: process context only
The following Jiurun Machinery channel video shows general automatic aluminum saw feeding. It does not demonstrate the setup-piece segregation, inspection release, material, machine configuration, customer job, trial outcome or production performance discussed here. Use it only to visualize a possible machine-and-part flow; demand a separate buyer-specific trial for the proposed route.
What should you ask before ordering?
Send the supplier your representative profile drawings, order mix and current first-piece release method. Ask them to identify every trial-piece destination and to show a changeover in which no unapproved piece enters the accepted batch. If the supplier can show the physical route and provide the agreed records, the buyer can judge the saw as part of a complete production process rather than a stand-alone cutting stroke. Contact JiurunCut with your part list and requested trial sequence for a scope discussion.