
A mixed aluminum-profile job can make a single saw-blade quotation look simple: choose a blade, cut a sample, and release the machine. The difficult question is whether that blade remains acceptable when the production mix changes. A clean result on one thick rectangular extrusion says little about a thin hollow section, an asymmetric T-slot, or a visible anodized face. A useful mixed aluminum profile blade trial therefore tests the intended family of parts, not a convenient showcase piece.
The goal is a buying decision, not a claim that one blade must cover everything. This guide shows how to build a small, controlled trial matrix, what to record, and when a second blade or a different fixture is the more honest quotation.
Define the profile family before discussing the blade
Start with the drawings and actual samples for the jobs the buyer expects the saw to run. Give each profile an ID. Record its alloy and temper if known, cross-section dimensions, minimum and maximum wall thickness, hollow chambers, visible finish, required cut angles, and which end faces matter in assembly. Flag profiles with an open side, long unsupported lip, internal web, or protective film. These details shape support and clamp access as much as blade choice.
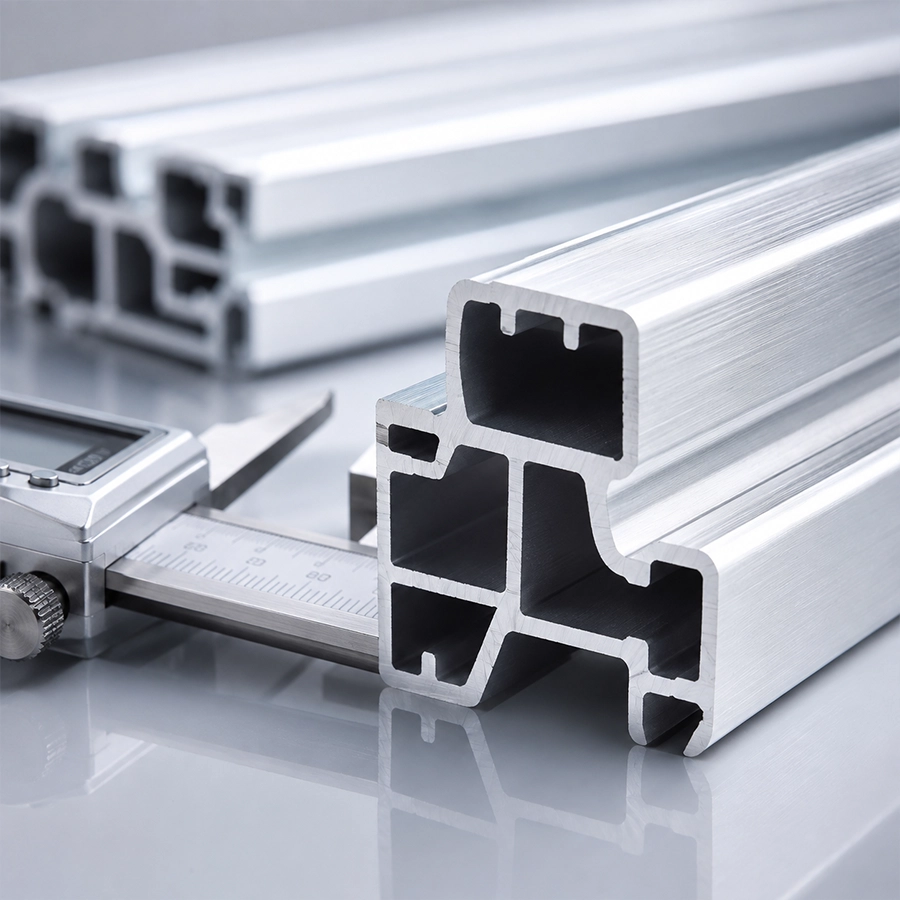
Do not assume every variation needs a separate blade. Equally, do not assume a shared nominal material makes the cuts interchangeable. The blade supplier’s application guidance can distinguish thin-walled aluminum profiles from other workpieces and may call for secure clamping; for example, LEUCO describes a specific nonferrous blade for thin-walled profiles and states its own application conditions. That page describes that manufacturer’s product, not a Jiurun machine specification or an automatic recommendation for your job.
Build a mixed aluminum profile blade trial matrix around buying risk
A short matrix is more useful than a large pile of unlabeled offcuts. It should include the easiest high-volume profile and the profiles most likely to challenge the proposed setup. If a visible finish or assembly end is the customer’s actual acceptance point, make it a named row. Record the planned number of repeat pieces for each row before the trial so that a single attractive cut cannot stand in for a stable process.
| Field | What the buyer should supply or agree | Why it matters |
|---|---|---|
| Profile ID and sample | Drawing revision, actual section, alloy/temper if known, finish and film | Prevents a result on a substitute section being treated as proof for production |
| Cut requirement | Angle, cut length range, end-face orientation and downstream fit | Connects blade and fixture choice to the real part |
| Acceptance method | Who judges burrs, marks, squareness, length and assembly fit; with what method | Makes pass/fail observable instead of subjective |
| Trial record | Blade identity, machine setup, support/clamp arrangement and repeat pieces | Lets the supplier reproduce and quote the tested condition |
Photograph or retain one labeled reference part per row. Keep the cutting orientation consistent with the production drawing, and identify the face that will remain visible after assembly. A smooth concealed face is not a substitute for a clean visible face.
Check blade fit before testing cut quality
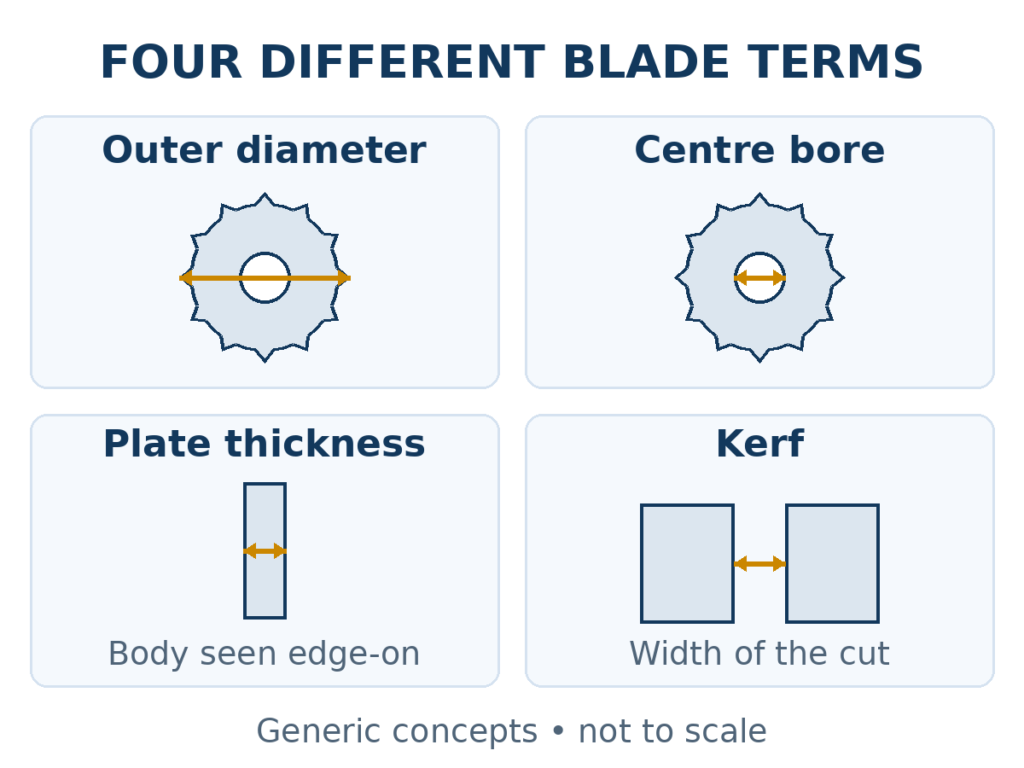
The proposed blade first has to fit the actual saw and its approved setup. Record its outer diameter, centre bore, body thickness, kerf, tooth count, tooth form, and supplier part number. Confirm the machine’s permitted blade envelope, rotation direction, guarding, flange fit, and spindle arrangement with the machine and blade suppliers. Do not treat a similar-looking diameter as compatibility. Our blade-dimension guide explains why outer diameter, bore, plate thickness and kerf are different terms.
Also agree who provides the trial blade, whether a new or used edge is being tested, and how it will be identified. The trial-blade supply checklist covers this ownership and record question. If the trial uses a blade that will not be supplied with the quoted machine, the quotation must say so.
Run the sections under a controlled setup
Begin with an agreed machine condition: blade identity and edge condition, coolant or lubrication arrangement if used, clamp pressure and contact points, stock support, stop position, feed setting and operator method. Record changes rather than quietly tuning each sample until it looks good. A hollow section may deform under a clamp that holds a solid section securely; a thin open lip may vibrate unless it is supported. That is a fixture or process finding, not automatically a blade failure.
Run a reference profile, then a challenging profile, then the reference again after the intervening cuts. This simple sequence helps reveal whether the first result was dependent on a fresh edge or temporary setup. For a family with several critical geometries, extend the matrix deliberately and note each configuration change. Ask for repeated parts, not only a video of one cycle. Retain rejected pieces with the same care as accepted pieces so the reason for a change remains visible.
Measure length and angle using the method agreed for the finished part. Inspect burr height or presence where handling and assembly matter, check chips or tearing at thin walls, and look for clamping dents or scratches on finished faces. Compare mating parts in their real assembly if fit is a requirement. Keep the saw’s feeding repeatability, an individual cut-end measurement, and final assembled fit as separate results; none is a synonym for another.
Interpret the result without overclaiming
If all required rows pass under one documented blade and fixture setup, request the same blade identity and consumable scope in the final quotation. If one section passes only with different clamp pads, support blocks, lubrication or feed settings, record that as a separate recipe and include the changeover work in the buying decision. If a second blade is needed, quote both blades and their changeover arrangement. If a profile has not been supplied or the acceptance method was not agreed, label that row untested.
When a supplier reports a blade’s maximum wall thickness or preferred use, read it as guidance for that exact blade and cutting context. Do not transfer a number from a blade catalogue to every saw or extrusion. Likewise, one favorable demonstration cannot establish blade life, cycle time, cut accuracy, or scrap rate over a production shift. Those claims require a separately designed trial and evidence.
What to put in the RFQ and acceptance record
Send the profile matrix with drawings and actual pieces, then ask the supplier to return a marked-up trial record. The record should identify the machine configuration, blade maker and part number, blade size and tooth design, stock support and clamping, settings for each profile, sample quantity, acceptance measurements, and every change made during the trial. Ask for photos of both good and rejected ends, including the visible face and any mating assembly. Separate the quoted baseline from optional blades, fixtures and consumables.
A practical RFQ sentence is: “Please evaluate whether one identified blade and one documented clamping arrangement can cut profiles A, B and C to the attached end-face and assembly criteria. If any row needs a different blade, support or setting, show the separate setup and quote its cost and changeover requirement.” This invites an honest result instead of forcing a yes-or-no promise before samples exist.
Illustrative media and next step
The images in this article are explanatory diagrams or representative views. They do not show this buyer’s parts or a completed mixed-profile trial. The video below shows general Jiurun equipment operation only; it does not prove a particular material, blade configuration, customer result, trial result or performance level.
Video caption: General JR-455CNC machine footage from Jiurun’s official YouTube channel. It is an equipment example, not evidence of the profiles, blade configuration, customer, trial cut or performance discussed in this guide.
If you are comparing aluminum cutting equipment, contact Jiurun with your drawings, profile samples, finish requirements and acceptance method. Ask us to define a witnessed trial matrix before choosing the machine, blade and fixture scope.
Frequently asked questions
Can one blade cut hollow, solid and T-slot profiles?
It may be possible for a defined range, but compatibility is a test result tied to a named blade, machine and setup. Do not infer it from material name alone. Include the hardest actual section and the required finish in the trial.
Is a good cut on one sample enough?
No. At minimum, identify the sample and repeat the critical cuts under recorded settings. A buyer should ask what happened after other profile types were cut and whether the same edge and fixture were used.
What if the supplier changes the blade during the demonstration?
Record the point of change and treat the subsequent result as a different configuration. Request both blade identities and the changeover procedure in the quotation, or repeat the matrix using the proposed production blade.