
Heat sink fin receiving inspection begins before a carton is opened. A buyer may approve the alloy, cut length and drawing, then discover at assembly that fine fins have been bent in transit or that a visually similar profile belongs to another revision. The purchasing decision is therefore about the accepted condition and identity of each delivered part, not simply whether a supplier can saw an extrusion.
This guide concerns cut aluminum heat-sink sections supplied for later manufacture or assembly. It does not set a universal fin tolerance, approve a thermal design, or claim that a photograph or machine video proves a particular shipment. Use the released drawing, agreed inspection method and actual distribution route as the controlling evidence.
Define the part and receiving stage first
Ask whether the order is for long extrusion stock, cut blanks, or finished heat sinks. A cut blank may still need machining, surface finishing or inspection by the buyer; a finished sink may have additional interfaces or coatings. The supplier and buyer must name the same handover point. Record the profile identifier, drawing revision, material and temper where specified, cut length, handedness or orientation if relevant, intended quantity per pack, and any subsequent operations. Do not use the overall enclosure or electronic product size as a substitute for the physical part drawing.
If several profiles look alike, make their package identity independent of visual recognition. Specify which members may share a carton, which must remain separated, and how a short shipment or replacement pack will be identified. A purchasing comparison should price the same accepted stage: a low saw-cut price and a higher ready-to-assemble price are not comparable until later finishing, inspection, packing and rejection costs are included.
Protect the fins without losing the base datum
The packaging concept should transfer support through surfaces the released part can tolerate. Ask the supplier to show where the load rests when a packed unit is stacked, carried and set down. A divider or tray can separate adjacent fin arrays; it should not press directly on the fragile edges it is meant to protect. The base, mounting face and cut ends may need a different contact treatment from the fins. Define any finish-sensitive face and residue restriction before choosing films, foam or interleaves. A generic “protective wrap” instruction is too vague to judge at receiving.
Choose the packaging unit according to the real order flow. Individually sleeved blanks can preserve identity but add unpacking work. A tray of one part number and revision can be efficient if parts cannot slide into each other’s fins. A mixed assembly kit may shorten picking, yet it needs an internal map so one damaged member does not make the whole kit untraceable. Ask for a drawing or annotated packing sample showing count, orientation, layer separation, lift points and label placement. This is a review request, not a prescribed universal pack design.

A packing trial must follow the actual route, not merely look tidy at a bench. Identify the parcel, pallet or dedicated rack flow, likely handling changes and intended receiver. ISTA explains that packaged-product test procedures challenge the product-and-package combination against distribution hazards. A buyer can use the applicable procedure or an agreed route-specific trial, but must decide the acceptance condition in advance; a test designation alone does not prove that a particular fin design arrived undamaged.
Write an incoming check that separates damage from variation
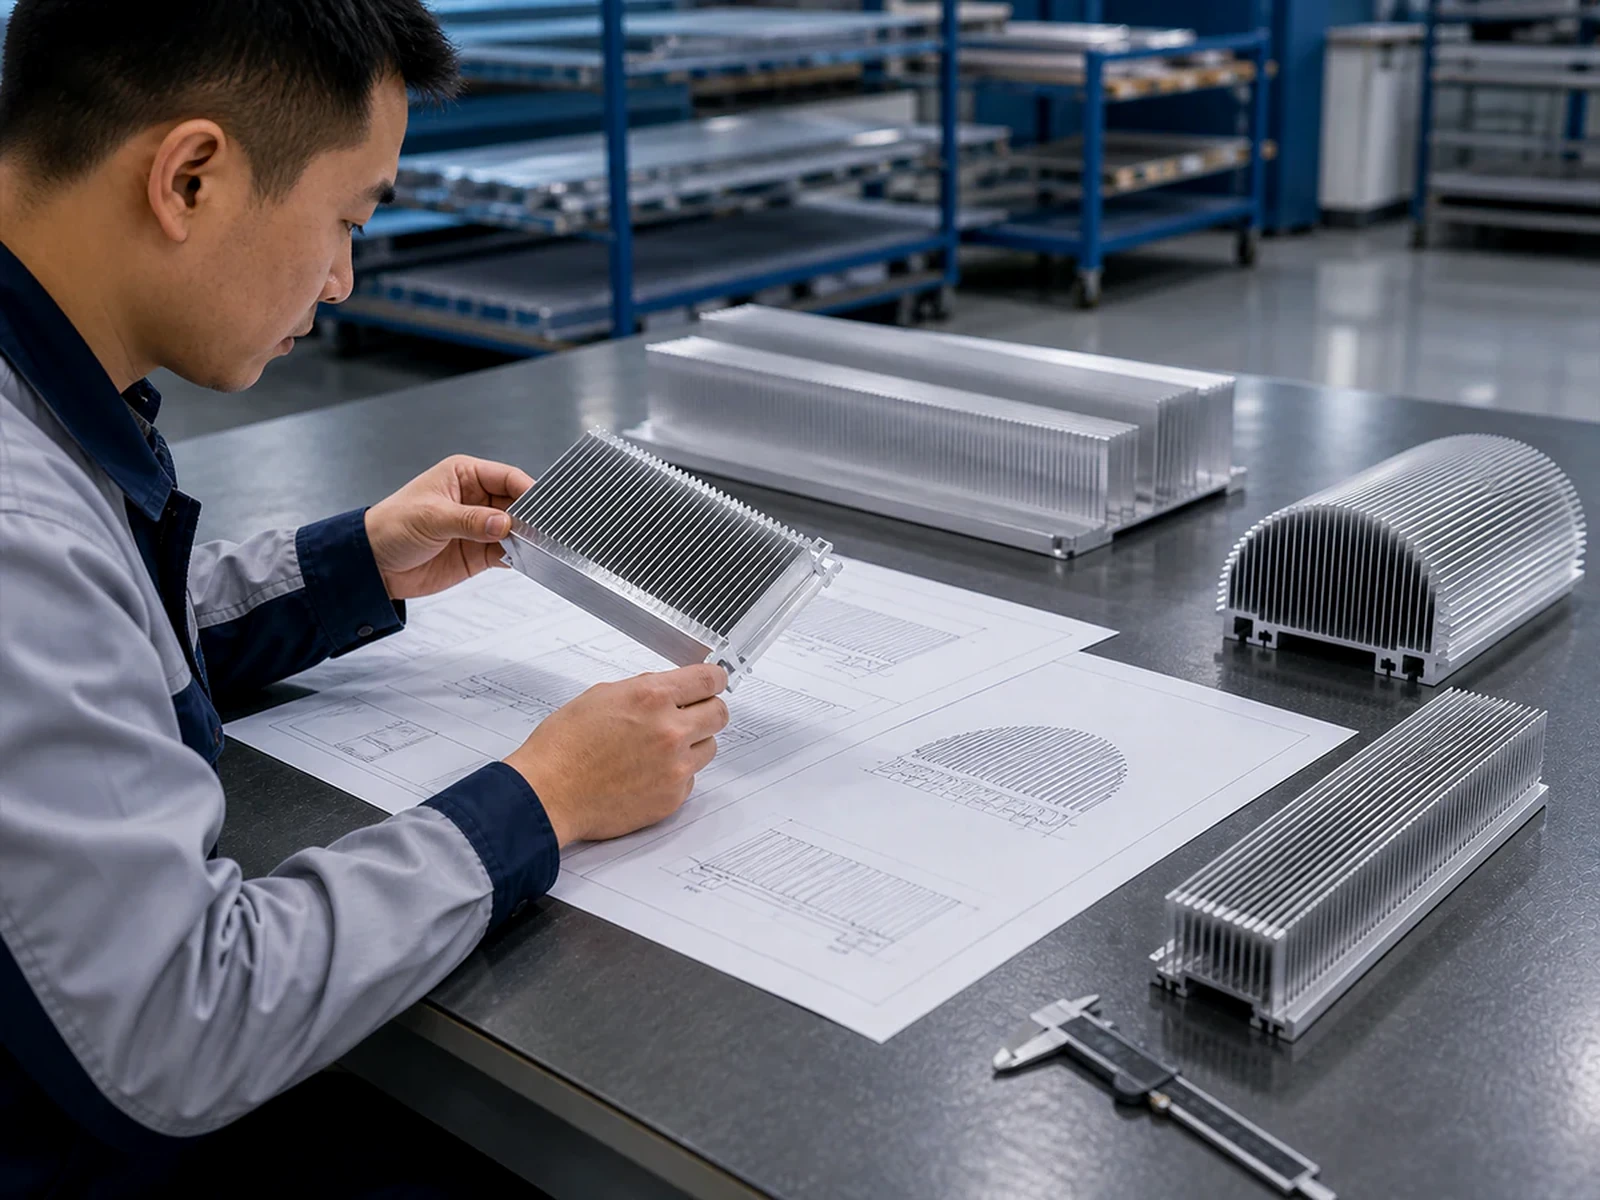
Before dispatch, agree where receiving staff may open a package and how they will preserve the label, internal separators and suspect piece. Inspect both the pack and the part. A crushed outer carton is a useful prompt for closer review, but an intact carton does not by itself prove every fin is acceptable. Check the released features relevant to the next operation: fin deformation or contact marks in nominated zones, cut-end condition, profile identity, visible surface condition and any base interface that the drawing controls. The buyer and supplier should decide which checks are visual, which require a fixture or instrument, and which require a retained reference sample.
Do not apply an invented fin-gap number to all heat sinks. Fin geometry, tolerances and permissible cosmetic marks differ by part and receiving stage. If the drawing is unclear, resolve the criterion before ordering production volume. Keep the saw-cut acceptance separate from thermal-system performance: a clean cut does not establish heat dissipation in the final product, and a thermal claim needs its own test and responsibility.

Define the disposition path as carefully as the inspection. A receiver should know whether to accept, segregate for engineering review, request a replacement, or return a lot; who may authorize any rework; and how an affected pack is linked to the shipment. Bending fins back by hand should not be an assumed repair. Record the actual defect location, part identity, count and photos with a reference scale where appropriate. This preserves the evidence for a supplier correction without presenting an isolated image as a statistically valid lot verdict.
Make labels useful after a carton is split
At minimum, the buyer’s receiving method needs the supplier’s part number, buyer part number where different, revision, quantity, lot or batch identity, and package sequence when an order spans multiple units. Decide whether these fields belong on every inner pack as well as the outer handling unit. The GS1 Logistic Label Guideline describes identification of logistic units and how human-readable and machine-readable information can work together; it does not replace the buyer’s component-level revision and inspection requirements.
A useful trial is to split a package as receiving really will. Can a worker identify one remaining piece after the outer label has been discarded? Can a replacement pack be matched to the same released part without guessing from appearance? If the answer is no, improve the inner-pack identification or the electronic packing record before expanding the order.
Compare bids on accepted, usable parts
Ask each bidder to quote the same drawing revision, receiving stage, order mix, pack quantity, transport route and inspection boundary. Separate the unit cut price from protective materials, packing labor, freight cube or weight effects, buyer unpacking labor, expected replenishment lead time and the handling of damaged parts. Do not manufacture a damage-rate promise from a single trial. Instead, use a small representative shipment to expose failure modes, revise the pack, then set an evidence-based release gate for the production lot.
For the trial, include the thinnest or most exposed fin family actually ordered, the shortest and longest relevant lengths, and any different finish or orientation that changes contact points. At the receiver, document pack condition before opening, verify identity and count, examine the agreed critical zones, and report both acceptable and unacceptable observations. Keep packaging test results, cut-part inspection and final thermal qualification as separate records. That distinction makes a supplier discussion much more precise than “the parts looked fine.”
Related decision: our mitered-profile packaging guide covers corner protection and matched-frame identity; heat-sink fins demand a separate contact and receiving check.
Video: general equipment context
The Jiurun Machinery channel video below shows general aluminum saw feeding and cutting equipment. It is included to illustrate the kind of upstream machine context a buyer may discuss. It does not show or verify the heat-sink profiles, packing method, machine configuration, customer order, trial shipment, cut quality, thermal performance or acceptance criteria in this article.
RFQ checklist for heat-sink fin receiving inspection
- Released profile and part drawings, revision, material condition, cut length and accepted supply stage.
- Named critical surfaces and fin zones, agreed inspection method, reference sample and separate thermal qualification owner.
- Pack layout showing support surfaces, separators, orientation, count, inner and outer identifiers, and handling assumptions.
- Distribution route and agreed packed-product or route-specific trial, with receiving observations and disposition rules.
- Quotation at one comparable accepted stage, including packaging, transport, incoming work and replacement responsibilities.
If you are evaluating an aluminum cutting route for finned profiles, contact JiurunCut with the released profile drawing, stock condition, cut-length range, order mix and receiving-stage requirements. We can discuss the cutting-machine scope to test; packaging and final product acceptance must be agreed against your actual parts and route.