
For aluminum sawing for turning, release the stock required by the confirmed receiving route. The same finished-part order does not automatically define the saw’s output. Establish the delivered item and the manufacturing stage at which it is handed over.
Aluminum sawing for turning
Fictional procurement example: a factory needs round aluminum spacers. Its designer and receivers have independently qualified two routes for that exact job. The finished-part requirement remains the same, but each receiver has released a different definition of its incoming material. These qualifications are premises of the example, not actual application approvals.
The first route accepts individual saw-released blanks. The second accepts approved feed bars. Purchasing initially copies the spacer order into a request for the same quantity of short blanks without saying which receiver will take them. That request commits to a physical delivery before the factory has chosen its receiving route.
DMG MORI distinguishes bar processing from handling individual billet workpieces.
In the fictional enquiry, both routes have been qualified independently; they are not assumed to be interchangeable on one machine. Selecting a receiver therefore fixes more than a destination. It determines what that receiver has agreed to accept, and that decision must reach the saw purchase before material is divided.
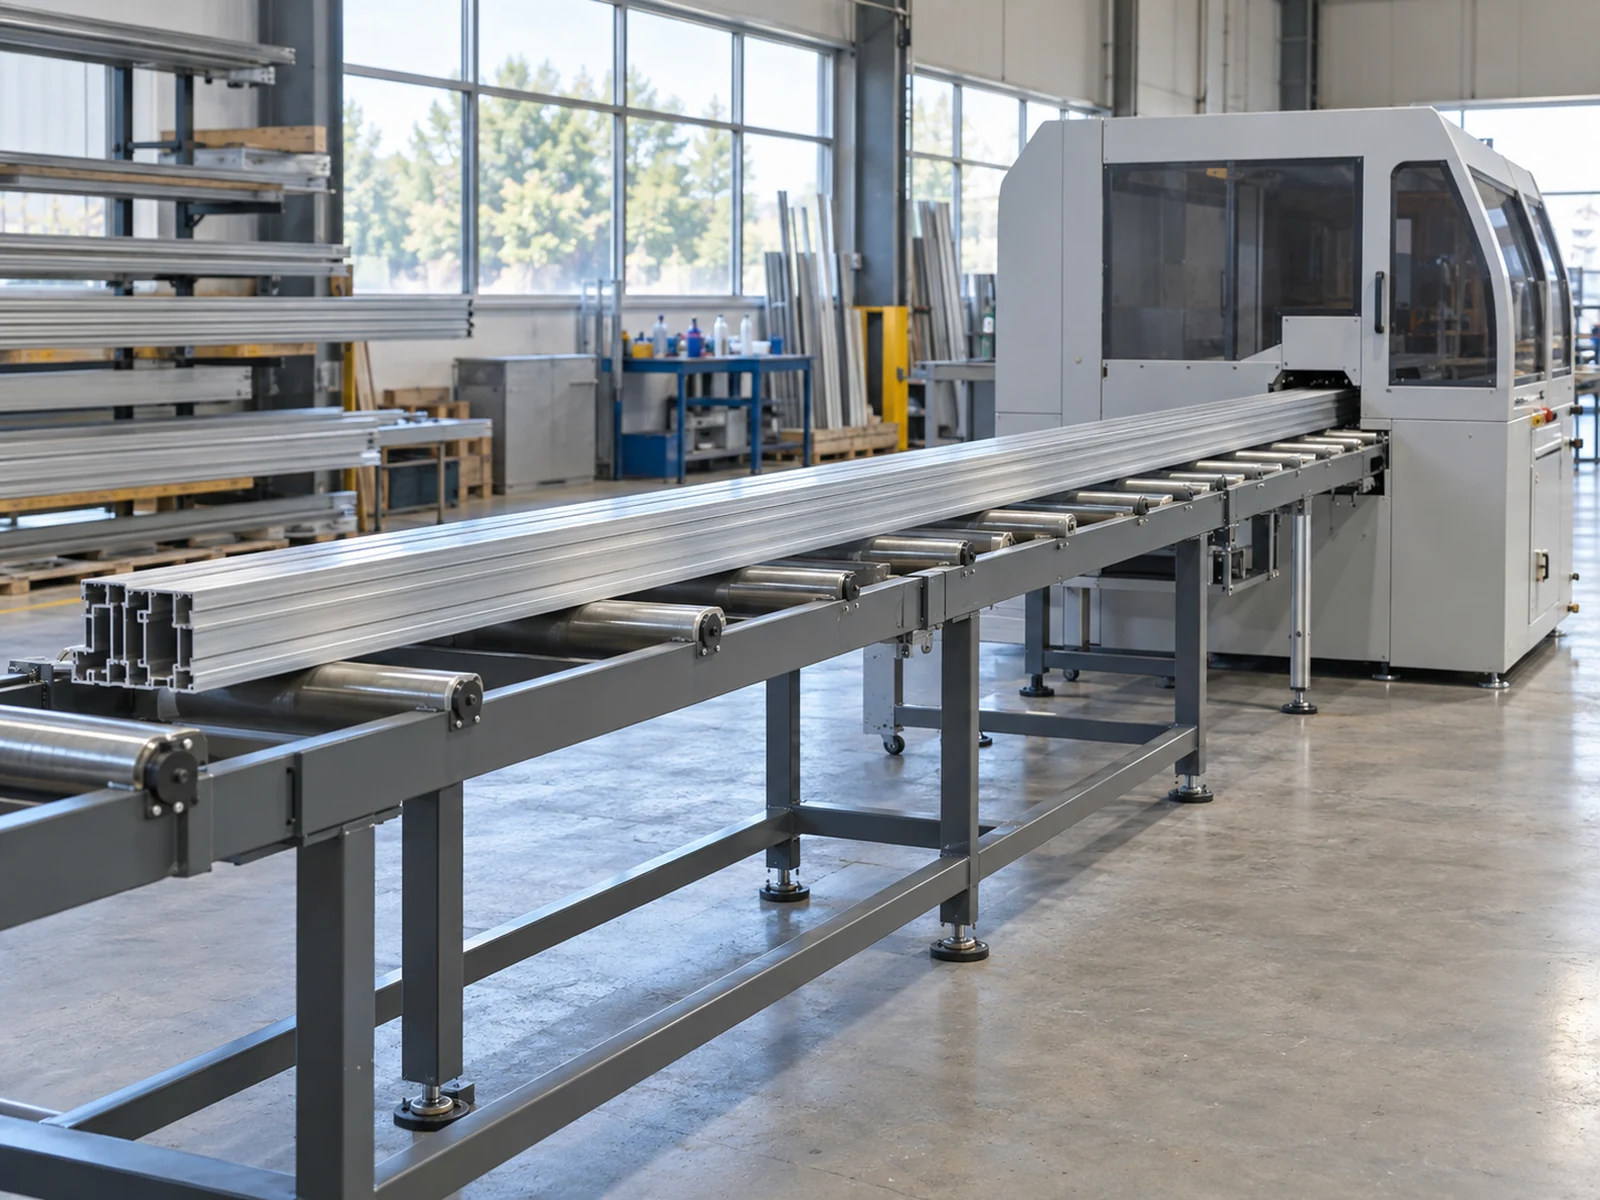
Separation
Haas links lathe parting-off with separating machined parts from bar-fed stock.
Blanks arrive separated; the feed-bar route leaves separation within the lathe. The purchase team therefore needs a route-specific description of its commitment, not a conversion of every finished spacer into an upstream short-piece order. Nothing about the final quantity decides that commitment for the factory.
Consider a supplier reply offering a quantity of individual blanks at the requested blank definition. It can answer the first receiving route without answering the second. It is not an inferior offer; it supplies a different input. A matching final production quantity does not make those short pieces the feed bars another receiver requested.
The feed-stock route may still involve sawing if purchased stock needs preparation to the receiver’s released condition. If the purchased stock already meets that condition and needs no saw work, preserve that possibility. Neither “a saw for every spacer” nor “no saw anywhere” follows merely from the route’s name.
Likewise, do not ask the cutting supplier to invent a feed-bar length from the finished spacer drawing. A blank definition and a feed-stock definition serve different receiving arrangements. The actual dimensions and preparation requirements remain with the confirmed route; this article provides no allowance or stock-utilization calculation.
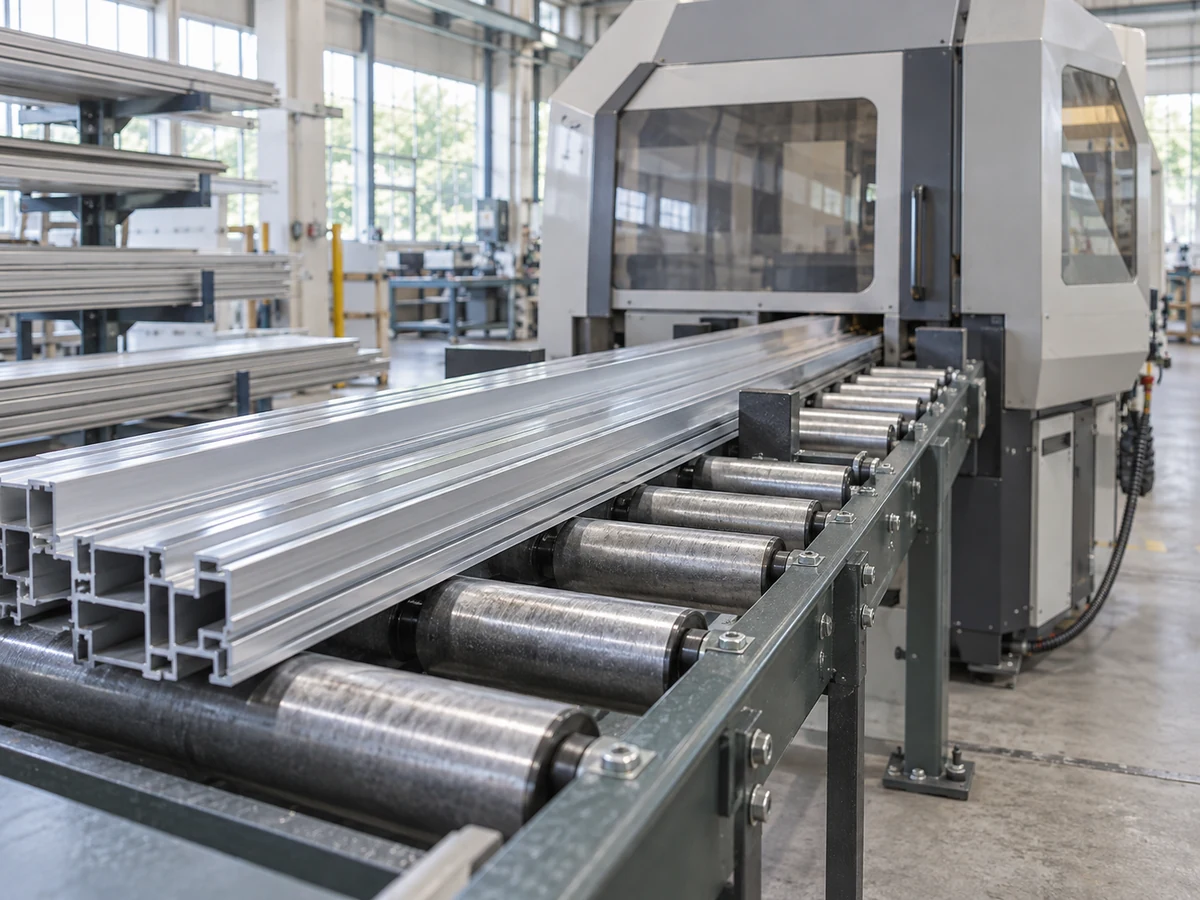
Handoff
The table follows the same spacer order to its two confirmed receiving routes. It compares physical handoffs, not machine types, recommended equipment or proven Jiurun capabilities.
| Input | Saw output | Remaining work |
|---|---|---|
| Blanks | Receiver-approved individual pieces. | Agreed machining of each blank. |
| Feed bars | Approved feed stock, if sawing is needed. | Successive machining and parting-off in the lathe. |
Sending longer stock to the blank receiver would leave its agreed input unprovided. Sending pre-cut blanks to the feed-stock receiver would also change the agreed delivery. Either recipient might assess another route, but purchasing cannot make that change on its behalf by treating all aluminum of the same specification as equivalent input.
The comparison deliberately leaves the number of spacers obtainable from a feed bar unspecified. That requires the actual receiving arrangement and its complete material plan. Counting delivered bars does not supply a finished-part count, just as counting individual blanks does not establish that every one has become an accepted finished spacer.
The saw supplier should therefore be asked to price and explain the actual stock task selected, not an ambiguous quantity of material “for spacers.” Comparing the two offers only at their saw-side delivery can hide work retained elsewhere. Keep the same finished-part objective visible without pretending that the intermediate objects are identical.
Commitment
For a repeat order on an unchanged receiving route, the existing valid input definition can give purchasing a clear starting point. There is no need to change to bars simply because the final parts are round, or to buy individual blanks because a saw is available. Neither route is inherently better in this example.
If the factory changes receivers, revisit the actual material handoff before reusing the old cutting order. That review may confirm the same supply, require a different saw task or remove upstream sawing for this job. None of those outcomes establishes a new machine requirement or a saving without the specific production plan.
Please quote the stock input released for our selected turning route, not one short piece per finished spacer by default. Distinguish any individual-blank preparation from feed-stock preparation, and keep downstream separation within the agreed receiving route. Where no saw operation remains, state that boundary clearly.
This keeps the equipment enquiry attached to a real input and output. It does not ask the saw supplier to choose a lathe process or approve bar-system compatibility. Those conditions belong to the receiving route and must already be clear enough to define the requested cutting work.
For equipment-category context, see the aluminum profile cutting machine and CNC aluminum cutting machine pages. These are circular-saw category references.
Discuss stock
Contact Jiurun with the actual aluminum stock, confirmed receiving route and released saw task. Identify whether the required delivery is an individual blank or feed stock, without assigning unconfirmed downstream work to the saw.
This article does not establish Jiurun turning, parting-off, robotic handling, line integration, engineering approval, trials or suitability for a particular stock and receiving arrangement.