
For aluminum transom cutting, decide whether the purchase ends with a saw-cut blank or with the final end shape required by the receiving frame profile. A shared member length does not establish shared contact geometry. Confirm where the blank becomes specific to that receiver before comparing the supplied work.
Aluminum transom cutting starts with the supplied end
Here, transom means the horizontal member within a frame. A profile-matched end means the end geometry specified for its contact with the receiving profile. It is not a strength classification, a sealing guarantee or the name of one mandatory machining method.
Hypothetical purchasing case: a producer makes frame variants R and S. Their nominal opening span and transom middle section are the same, but their approved drawings specify different receiving-profile contours where the transom meets the frame. The factory is considering common saw-cut blanks finished downstream or members supplied with their respective final ends.
R and S are invented design labels, not customer names or machine models. The example assumes the contact contours genuinely differ. Different receiving-profile product codes alone would not establish that different transom ends are necessary.
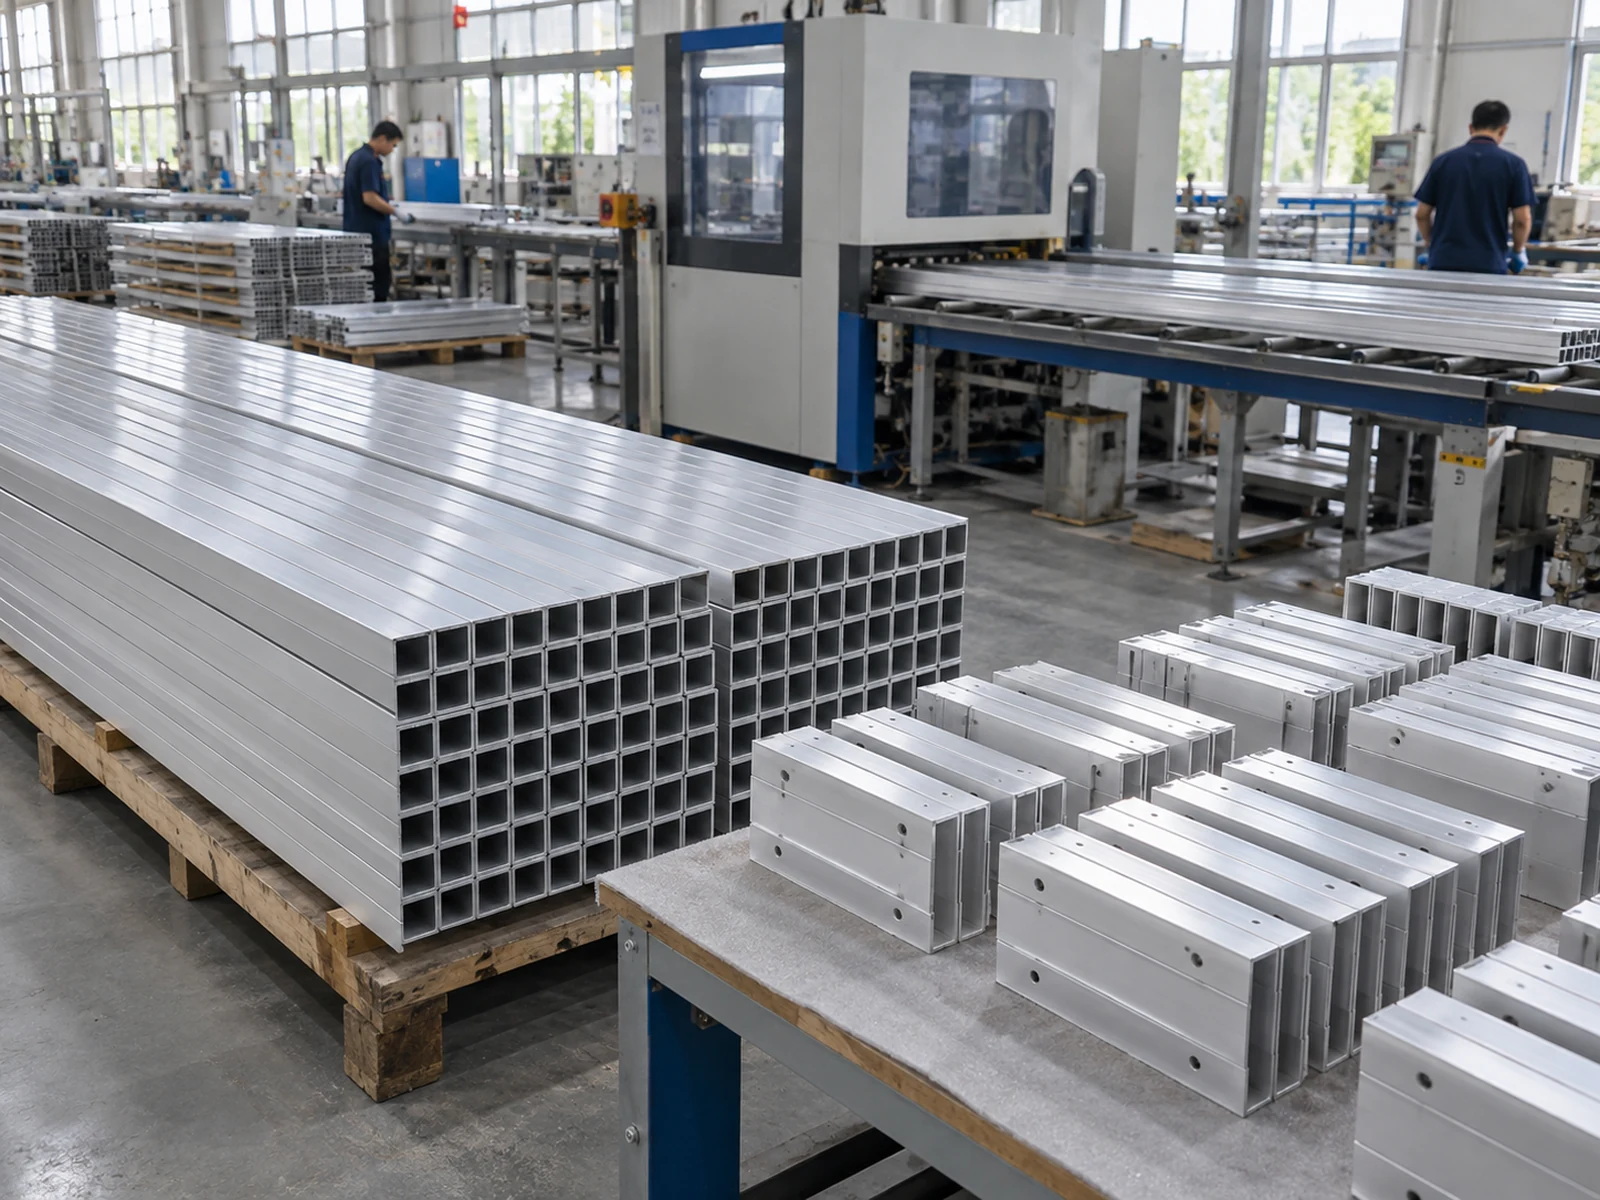
elumatec’s end-milling category page describes equipment for machining aluminum and PVC profile ends used in window and door joints. The separate end-preparation stage in this article is our purchasing interpretation, not a universal instruction from that manufacturer or evidence of a JiurunCut function.
A shared span does not make R and S interchangeable
Compare the intended contact region, not just the distance the transom spans. In the fictional case, a member prepared for R does not become an S member because its middle section and nominal length match. Its end still has to correspond to S’s specified receiving contour.
Keep the incoming blank and the final member distinct in the discussion. A supplier saying that both are cut to the same length may be describing a legitimate common intermediate piece. That answer has not established that the piece has either final contact end.
The distinction also matters when reading a finished-part drawing. Ask the responsible manufacturing party to relate its blank definition to the final ends for each variant. Do not copy the final member’s length into the blank request without that connection, or assume later contour work leaves every length reference unchanged.
No allowance is selected here. The actual drawings and proposed route must establish what material needs to remain for either finished shape. If that has not been resolved, call it a proposed common blank rather than an interchangeable input already confirmed for R and S.
Choose where the blank becomes receiver-specific
Route A begins only after common-blank suitability is confirmed. The factory buys or makes that saw-cut input, then its appointed downstream provider produces the R or S end. The material remains common only until the respective contact shape is made; the shared blank does not remove the need for that later capability.
Route B purchases the differentiated member. The supplier’s output already has the specified R or S end. The buyer receives a receiver-specific part rather than a blank awaiting that operation. Any remaining work still follows the actual finished-member definition; the end contour alone does not mean the entire joint is ready for installation.
To avoid treating more machining as automatically better, add a fictional design T. Its approved joint uses a straight final end and a different connection arrangement. T needs no extra contour operation merely because R and S do. Whether the saw output is already T’s final end must still be confirmed against T’s drawing.
| Physical output being purchased | Work remaining for the specified member | Production tradeoff |
|---|---|---|
| Confirmed common saw-cut blank for R and S | The appointed downstream route forms the required receiver-specific ends. | One intermediate input can serve either version only while both final shapes remain achievable. End preparation is still work to provide. |
| Finished end for receiver R or S | Only the further operations identified for that particular member; they are not presumed included. | The delivered end is already specific to its receiving contour. Common span and section do not establish interchangeability. |
| Straight final end for approved design T | No added contour work solely because another design requires it. | Buy the output T actually needs, subject to confirming that the stated saw result satisfies its end definition. |
A factory with a confirmed end-preparation route can evaluate buying only the common blank. Without that route, it has not solved the R/S requirement by procuring more blanks. Conversely, receiver-specific ends may remove that stage from its own work, but are not inherently a cheaper or more flexible purchase.
Keep the saw purchase aligned with the confirmed handoff
YILMAZ’s KM 211 S product description identifies a manually operated machine for aluminum-profile end milling. This is an example of a named end-machining process, not confirmation that the machine suits fictional R or S or that JiurunCut supplies the same work.
Neither cited equipment description decides this factory’s route. Do not conclude that every transom needs end milling or that a circular saw can never produce a required end feature. Assess the actual shape and configuration, without making a general machine category substitute for that answer.
A useful buyer reply can address the decision directly:
R and S share the transom section and nominal span, but the approved contact-end contours differ. Please state whether your output is a blank confirmed for both downstream routes or a finished end specific to R or S. Identify the end preparation left outside the offer. For T, assess its approved straight-end requirement separately rather than adding the R/S operation.
This separates an incomplete response from an unsuitable proposal. A blank-only answer can be sufficient for a buyer that has the remaining work assigned. It is incomplete for a buyer expecting receiver-specific final ends unless that difference is resolved before the purchase.
Send the input and the end state you need to receive
Share the actual aluminum transom section, incoming state and approved receiving-profile geometry with JiurunCut. State whether the saw should supply an intermediate blank or the required final end, and which later work is already assigned.
Contact Jiurun About Your Transom Cutting Scope
Suitability for the particular end shape remains to be assessed. This article does not establish JiurunCut end-milling, profiling, tooling, combined fabrication or trial services, and it does not approve joint strength or sealing performance.