
Aluminum residual stress is an internal material condition, while bow, twist and flatness are geometric observations. If a blank or machined part changes shape, record the geometry first and investigate the cause separately. A straight-looking piece is not a residual-stress test, and a bent piece does not identify one cause by itself.
This guide explains how to turn an observation into a useful engineering review. It focuses on the evidence needed when purchasing cut aluminum blanks or coordinating later machining. It does not prescribe a heat-treatment cycle or a universal cutting adjustment.
Aluminum residual stress: what the term means
TWI describes residual stresses as stresses that balance within a component and arise from incompatible internal strains. They can be created or changed during a component’s life. This is different from an external load currently applied by a clamp or an assembly.
For machining, distinguish the incoming material condition from the condition introduced by an operation. Weber and colleagues’ aluminum milling study separates initial bulk residual stresses in the blank from machining-induced residual stresses. The study concerns particular specimens and machining conditions; its results are not a performance guarantee for every aluminum cut part.
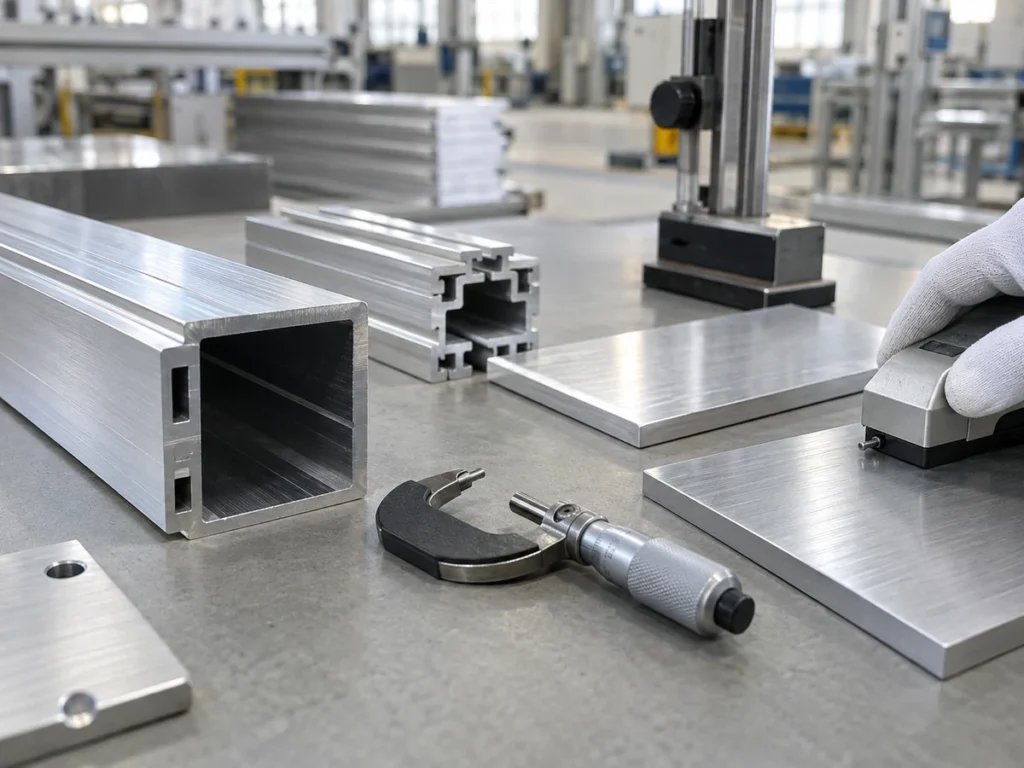
Step 1 — preserve the first observation
Replace “the aluminum moved” with a specific record. Identify the part, drawing revision, observed feature and stage of manufacture. State whether the observation concerns a cut blank, a machined pocket, a released component or an assembled product.
Describe how the piece was supported and whether it was restrained during the measurement. If two readings were taken under different conditions, keep both conditions beside the results. Do not average them together and lose the difference that needs investigation.
Include the tool or measurement method, datum and relevant inspection conditions required by the agreed plan. A photograph can help show orientation or support locations. It should supplement the recorded observation rather than become the only evidence.
A simple observation format
Use a short sentence with five fields: “Part identity — operation stage — feature — measurement condition — observed result.” Leave the cause field open until someone has reviewed the evidence.
For example, a fictional workshop note might say: “Part K12, revision B — after pocket machining — mounting face — measured in the released condition — see inspection record R7.” This is an example of record structure, not an actual result or a residual-stress measurement.
Step 2 — separate the starting blank from later operations
Keep the complete material description with the part. Preserve alloy, temper, product form, source record and any relevant lot reference. A shortened material name can remove information that the reviewer needs to understand the incoming condition.
Next, create a compact operation history. List the cutting stage, subsequent machining, joining and other relevant steps actually performed. Mark where the observed geometry was first recorded. Do not add assumed processes merely because the finished shape looks familiar.
| Record | Question it helps answer |
|---|---|
| Incoming material identity | What stock and condition entered the job? |
| Operation history | What happened before the observation? |
| Inspection condition | How and at which stage was geometry checked? |
The distinction between initial and machining-induced stress is useful for organizing a review. It is not permission to assign every change to either the mill or the machine operator without evidence. Keep the material history and manufacturing history available to the same reviewer.
Our 6061-T6, T651 and T6511 comparison explains why the full material condition belongs in a purchasing record. Retaining that condition does not replace acceptance of the finished component.
Step 3 — choose evidence that answers the actual question
If the question is “does this mounting face meet the drawing?”, use the agreed geometric inspection. If the question is “what is the residual-stress state here?”, have a specialist select an appropriate stress-evaluation method and scope. Those are different deliverables.
TWI lists methods ranging from diffraction techniques to hole drilling and destructive sectioning. Its overview also notes limitations in both measurement and prediction. A method name alone is therefore not a complete test plan.
Ask the specialist to define the location, direction and depth range represented by a result. Confirm whether the evaluation changes or consumes the sample, what preparation is required and how the findings will be reported. Keep these questions tied to the actual component and the purpose of the review.
Do not turn one local reading into a statement about an entire batch unless the approved evaluation plan supports that conclusion. Similarly, a computed stress field should have an identified model and review basis. A colored plot without that context is difficult for a buyer to use responsibly.
What the purchasing team can request
- A clear statement of the question the evaluation will answer.
- The sample identity and relationship to the production parts.
- The proposed method, covered region and reporting scope.
- The technical owner who will interpret the result and approve the disposition.
These fields let purchasing coordinate the work without pretending to perform the specialist analysis. Agree them before the test order so the final report addresses the project question.
Step 4 — approve the next action without losing traceability
If a material change, revised machining sequence or corrective process is proposed, send it to the responsible technical authority. Keep the proposal separate from the original observation. Record what was approved, which parts it covers and what follow-up inspection is required.
A request to “remove all stress” is not a useful universal acceptance instruction. Ask for the actual material, dimensional and functional requirements instead. Do not prescribe a generic heating cycle or assume that waiting for a fixed number of hours will solve the problem.
After an approved change, compare results using the defined inspection conditions and stage. Preserve the earlier record so the team can understand what changed. If the manufacturing scope changes again, return the new proposal for review rather than extending an earlier approval by assumption.

Common questions
Does acceptable flatness mean there is no residual stress?
No. Flatness is a geometric requirement. A stress-evaluation question needs its own method and scope. Keep the two results separately identified.
Can every bowed aluminum blank be blamed on residual stress?
Record the actual condition and have the evidence reviewed. Shape alone does not establish the cause, the contributing operation or the approved remedy.
Does a stress-relieved material designation approve final machining?
Preserve the material condition, then review the actual manufacturing and finished-part requirements. The designation does not replace a final geometric inspection.
What should I send for an aluminum cutting review?
Provide the stock drawing, full material condition, cut lengths, quantities and blank acceptance requirements. Include any approved downstream allowance and identify the stage at which each dimension applies.
Make the cutting handoff clear
Read our guides to flatness versus parallelism and welding distortion for related but separate geometry questions. Keep their requirements connected to the appropriate operation stage.
Send JiurunCut the aluminum blank drawing and cutting requirements to discuss the cutting scope. If a residual-stress investigation is required, keep the evaluation and disposition with the responsible material or manufacturing specialist.
Technical reading: TWI — Residual stress; Weber et al. — Machining-induced residual stress and distortion in aluminum workpieces.